HDPE Blown Film: Durable Packaging Solutions

Let Us Help You with Pricing

Our sales team will contact you shortly with pricing details and suggestions.
Name
Company Name
Email
Mobile
Message
0/1000

hdpe blown film

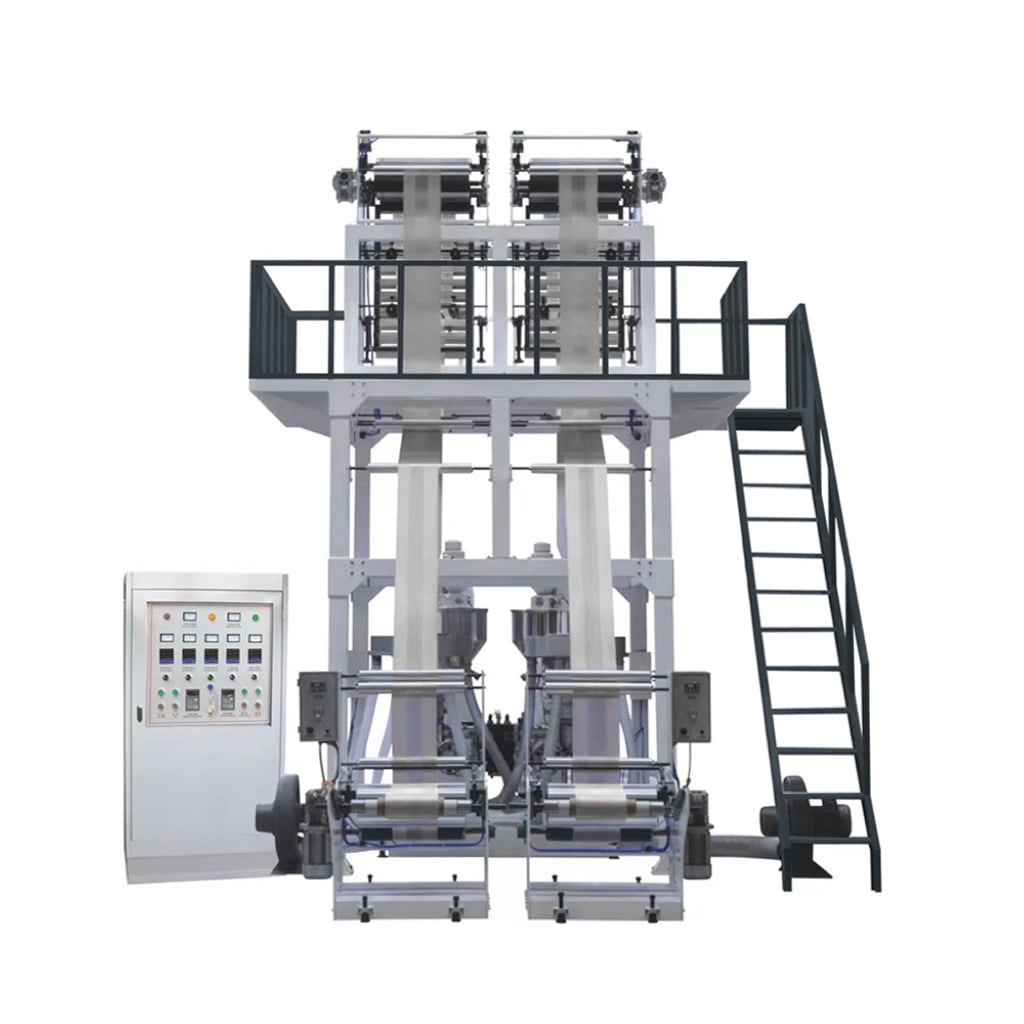
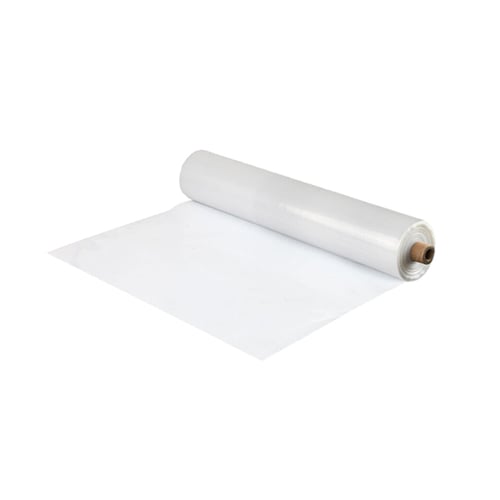
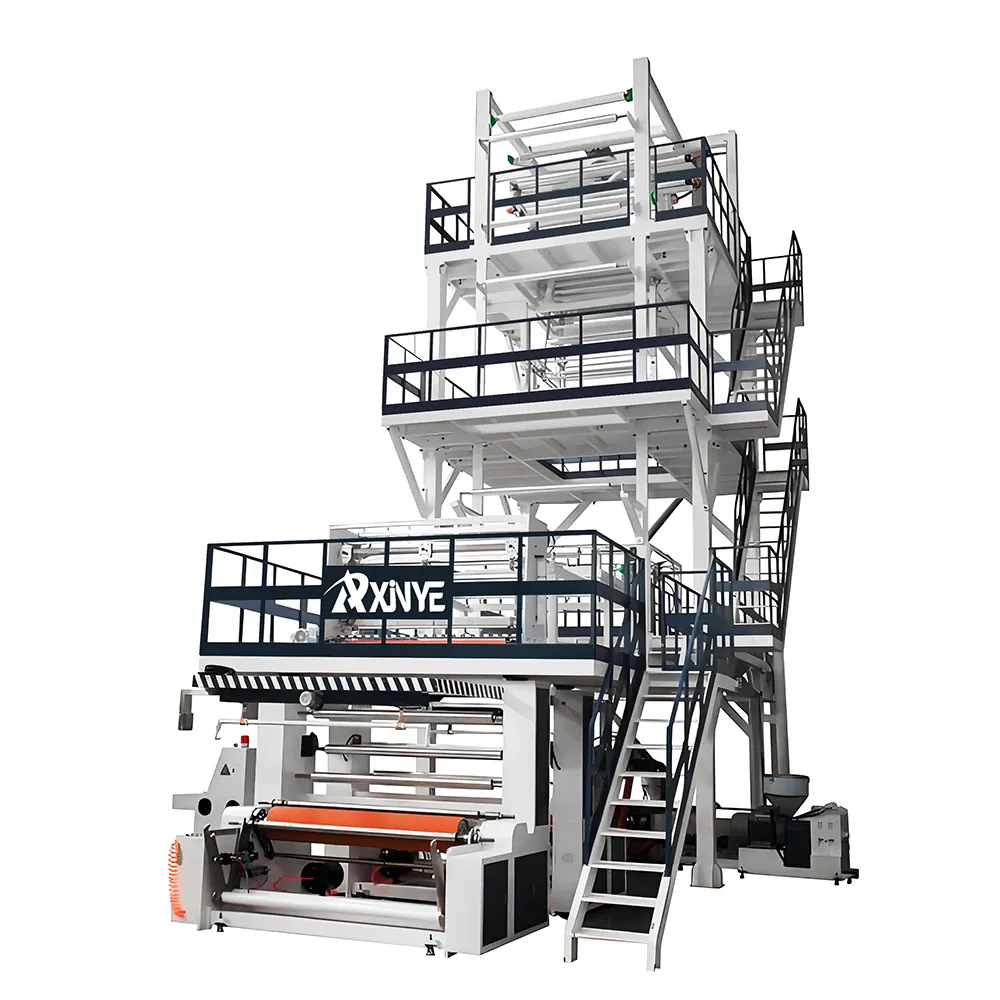
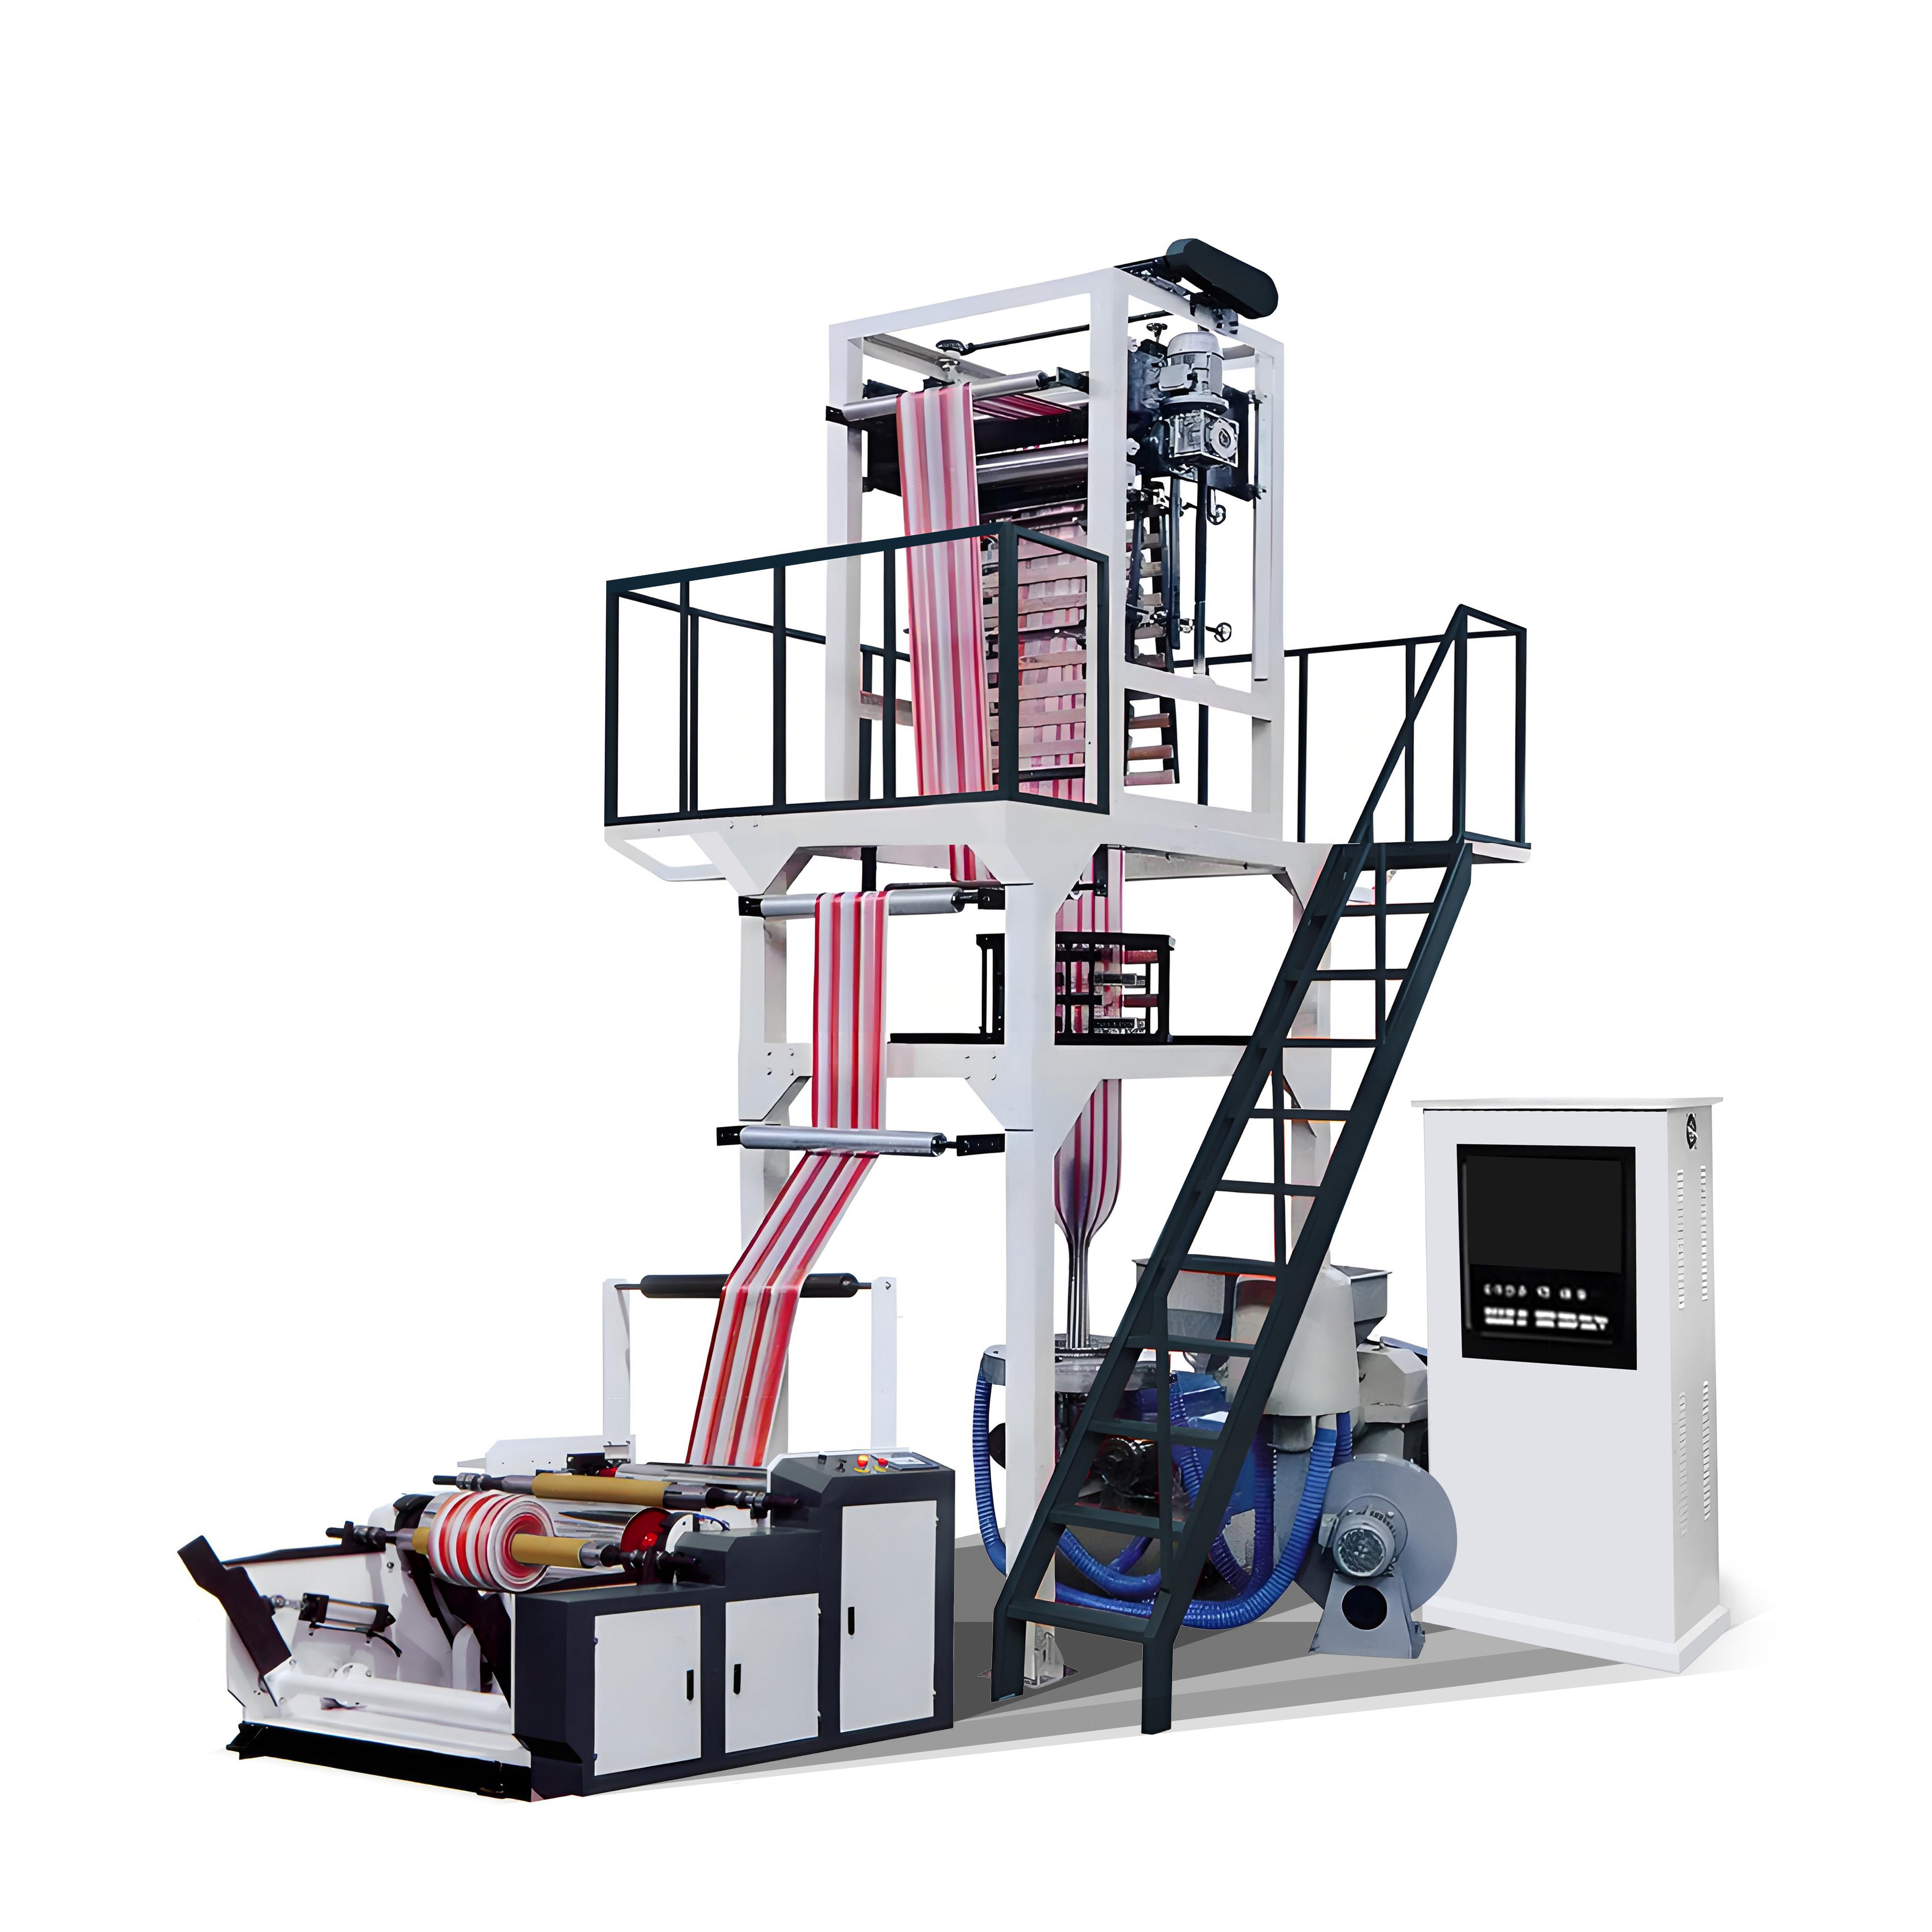
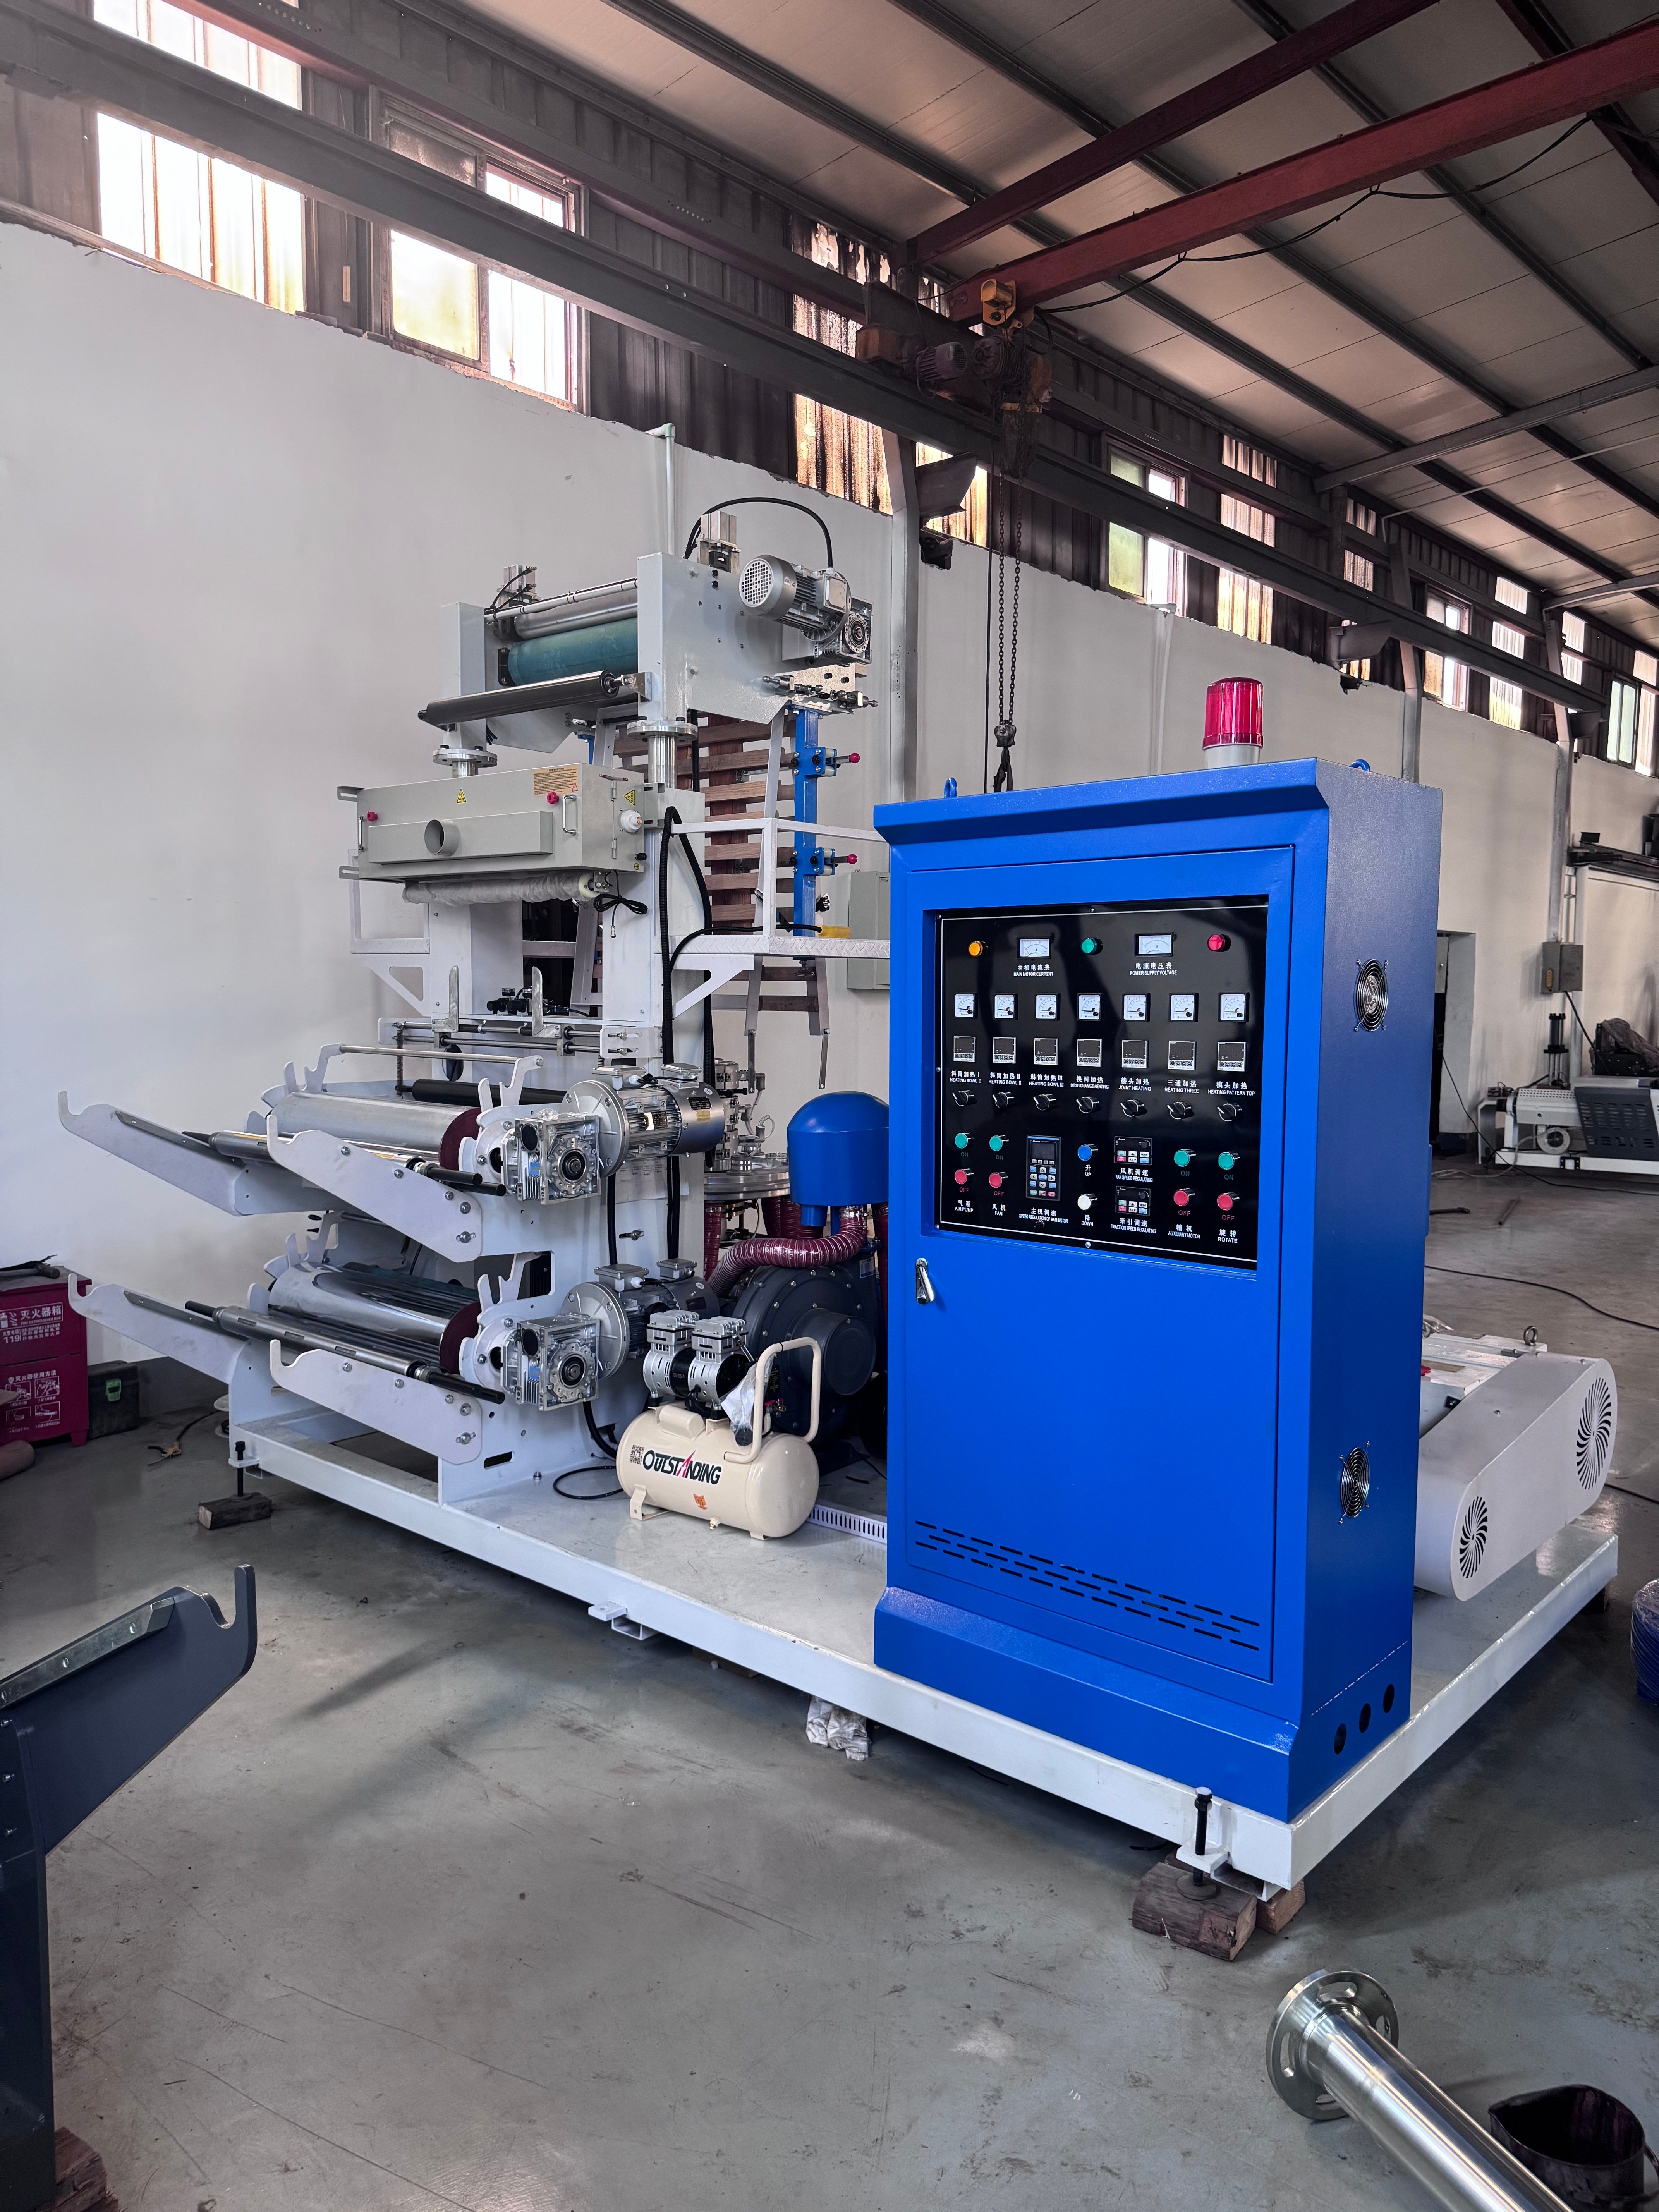
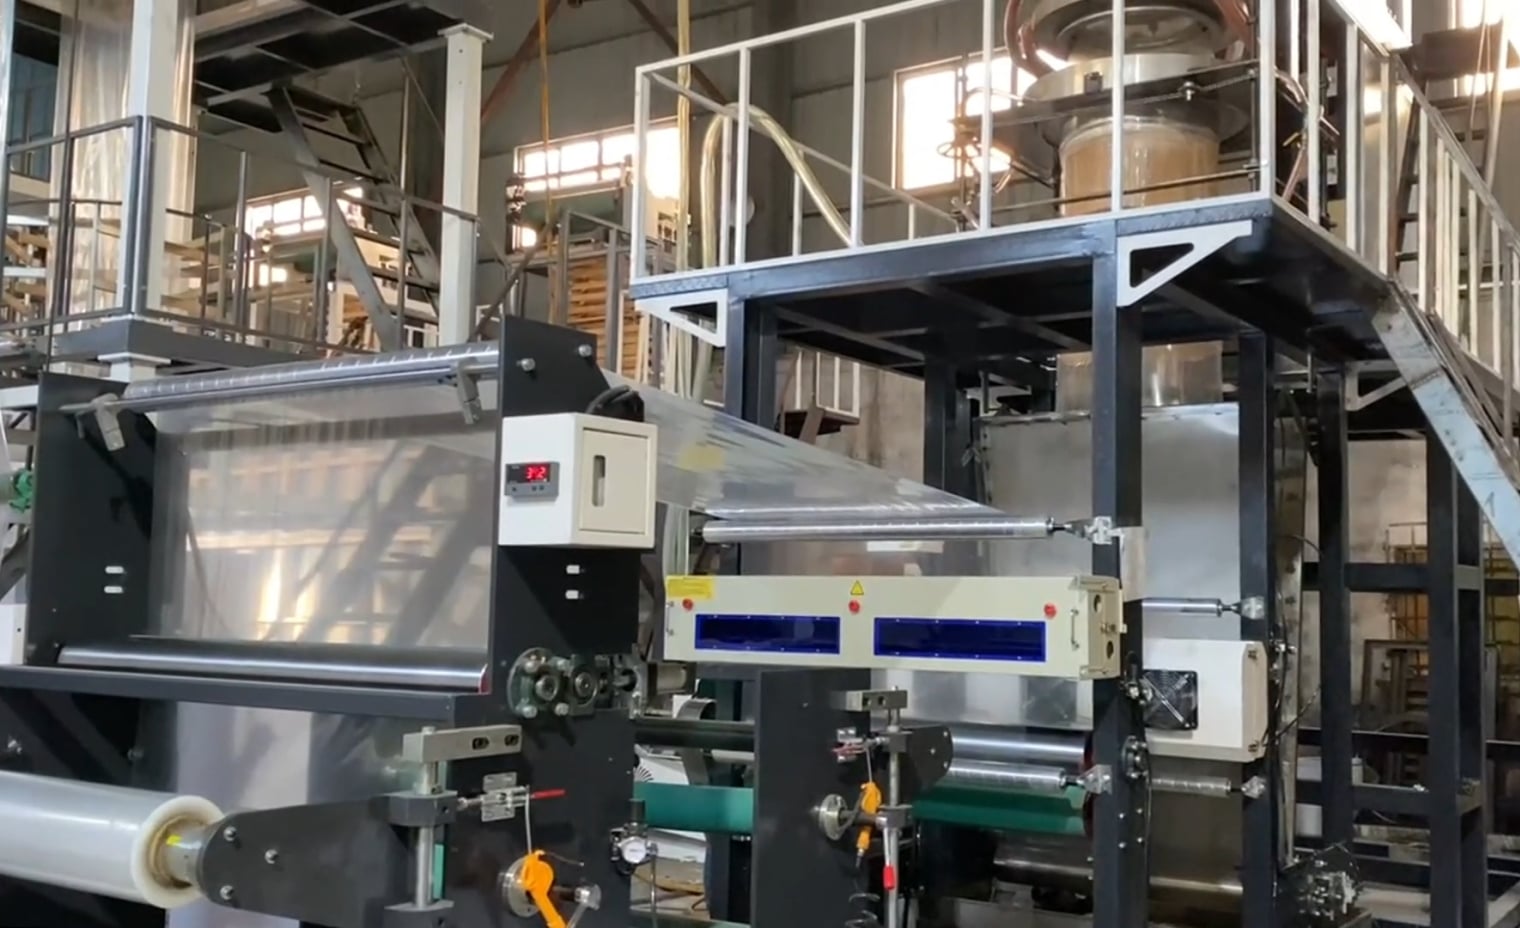
HDPE blown film represents a versatile plastic film solution manufactured through advanced extrusion and blow-molding technology. This high-density polyethylene material delivers exceptional performance across diverse industrial and commercial applications. HDPE blown film is produced by forcing melted polymer through a circular die, which creates a bubble that expands and cools into thin film sheets. The main functions of HDPE blown film include protecting products from contamination, moisture, and environmental damage while maintaining structural integrity. HDPE blown film excels in applications requiring flexibility, transparency, and durability. The technological features of this material include superior tensile strength, puncture resistance, and low permeability to oxygen and moisture. Key technological advantages include the film's ability to withstand extreme temperatures and mechanical stress without compromising performance. HDPE blown film accommodates various thickness specifications, allowing customization for specific application requirements. The manufacturing process enables consistent quality control and reproducibility across production batches. Applications span multiple industries, including food packaging, agricultural films, industrial wrapping, and protective coverings. HDPE blown film serves the retail sector for bags and packaging materials, while agricultural industries utilize it for greenhouse applications and storage solutions. The material's recyclability makes HDPE blown film an environmentally conscious choice for manufacturers seeking sustainable packaging alternatives. Its widespread adoption reflects the material's reliability, cost-effectiveness, and adaptability to modern production demands across global markets.
New Products

HDPE blown film delivers practical benefits that directly impact your operational efficiency and product quality. The material's exceptional durability ensures your products remain protected throughout storage and transportation, reducing damage-related losses and customer complaints. This reliability translates into measurable cost savings for your business. Operationally, HDPE blown film offers straightforward processing capabilities that integrate seamlessly with existing production equipment. The film's consistent properties enable predictable performance, eliminating production uncertainties and allowing precise quality control. Your manufacturing team will appreciate the material's stability during high-speed application processes. For packaging applications, HDPE blown film provides superior barrier properties that extend product shelf life while maintaining product integrity. The material resists punctures and tears effectively, protecting contents from external contamination and environmental hazards. This protective performance reduces wastage and enhances customer satisfaction. The versatility of HDPE blown film makes it suitable for diverse applications ranging from food packaging to agricultural use. Whether you need transparent films for visibility or opaque options for light protection, this material adapts to your specific requirements. The film's flexibility enables custom thickness options that match your exact specifications and budget constraints. Cost-effectiveness represents another significant advantage for manufacturers and packaging businesses. HDPE blown film delivers premium performance without premium pricing, making it economically attractive for high-volume operations. Additionally, the material's recyclability supports your sustainability initiatives while maintaining production efficiency and meeting environmental regulations effectively.

Latest News

The Role of Film Thickness Control in High-Quality Blown Film Production

31

Jan

The Role of Film Thickness Control in High-Quality Blown Film Production

Why Film Thickness Control Is Fundamental to Blown Film Quality How thickness uniformity directly determines mechanical strength, optical clarity, and barrier performance Getting film thickness just right matters a lot for blown film quality becaus...
View More
How Automatic Thickness Control Systems Work in Film Blowing Machines

25

Feb

How Automatic Thickness Control Systems Work in Film Blowing Machines

Core Principle of Film Blowing Machines: Closed-Loop Feedback for Real-Time Thickness Correction At the heart of precision in film blowing machines lies the closed-loop feedback system—a dynamic process where thickness measurements directly ...
View More
Tower Design Considerations in High-Speed Film Blowing Equipment

25

Feb

Tower Design Considerations in High-Speed Film Blowing Equipment

Structural Integrity and Dynamic Stability of the Film Blowing Tower Managing Dynamic Loads and Vibration at High Line Speeds When running at over 100 meters per minute, film blowing towers encounter all sorts of dynamic problems that can really s...
View More
Managing Tensile Strength in Blown Film Machines for Durable and Reliable Packaging Film

27

Mar

Managing Tensile Strength in Blown Film Machines for Durable and Reliable Packaging Film

Why Tensile Strength Is the Core Performance Indicator for Packaging Film Linking tensile strength to real-world packaging demands: puncture resistance, seal integrity, and load retention When it comes to packaging films, tensile strength matters m...
View More

Let Us Help You with Pricing

Our sales team will contact you shortly with pricing details and suggestions.
Name
Company Name
Email
Mobile
Message
0/1000

hdpe blown film

Superior Puncture and Tear Resistance

Superior Puncture and Tear Resistance

HDPE blown film exhibits outstanding puncture resistance that protects your products from accidental damage during handling, storage, and distribution. The material's molecular structure provides inherent strength that prevents small punctures from developing into larger tears, maintaining package integrity throughout the supply chain. This exceptional durability significantly reduces product loss and customer dissatisfaction caused by damaged packaging. The tear resistance of HDPE blown film enables safe handling in demanding environments without compromising film performance. Whether products encounter sharp corners, rough surfaces, or mechanical stress, the film maintains its protective barrier. This robust performance proves invaluable for industries requiring reliable protection, including food processing, electronics distribution, and industrial applications. HDPE blown film's resistance characteristics ensure your products reach customers in pristine condition, enhancing brand reputation and customer loyalty. The long-term cost benefits of reduced damage make HDPE blown film an economically smart investment.
Excellent Moisture and Oxygen Barrier Properties

Excellent Moisture and Oxygen Barrier Properties

HDPE blown film provides exceptional barrier protection against moisture and oxygen transmission, essential for preserving product freshness and quality. The material's low permeability prevents external moisture from penetrating packaging, safeguarding contents from humidity-related degradation. This barrier capability extends shelf life for perishable items, pharmaceuticals, and sensitive products requiring protective environments. Oxygen barrier properties of HDPE blown film prevent oxidative degradation that compromises product integrity and appearance. Food manufacturers particularly benefit from these protective characteristics, as oxygen infiltration accelerates spoilage and discoloration. The film's molecular composition creates an effective shield against atmospheric gases while maintaining optical clarity for product visibility. HDPE blown film's barrier excellence reduces waste caused by premature product degradation, directly improving your profit margins. Industries relying on extended product shelf life—including food, pharmaceuticals, and electronics—consistently choose HDPE blown film for dependable performance and consistent protection standards.
Versatile Customization and Sustainable Material Choice

Versatile Customization and Sustainable Material Choice

HDPE blown film offers exceptional customization capabilities, allowing manufacturers to specify exact thickness, width, and optical properties for unique application requirements. This flexibility enables businesses to optimize material usage and production efficiency without compromising performance or quality standards. Custom formulations accommodate specialized applications ranging from transparent packaging to pigmented films with enhanced barrier properties. The material's sustainability credentials make HDPE blown film an environmentally responsible choice for forward-thinking manufacturers. HDPE blown film's recyclability supports circular economy initiatives while maintaining premium performance characteristics. Many industries increasingly prefer HDPE blown film due to its reduced environmental footprint compared to alternative packaging materials. The film's durability minimizes replacement frequency, reducing overall material consumption and waste generation. Choosing HDPE blown film demonstrates corporate environmental commitment while delivering practical business benefits through reduced material costs and waste management expenses.