Blown Polyethylene Film: Durable Packaging Solutions

Let Us Help You with Pricing

Our sales team will contact you shortly with pricing details and suggestions.
Name
Company Name
Email
Mobile
Message
0/1000

blown polyethylene film

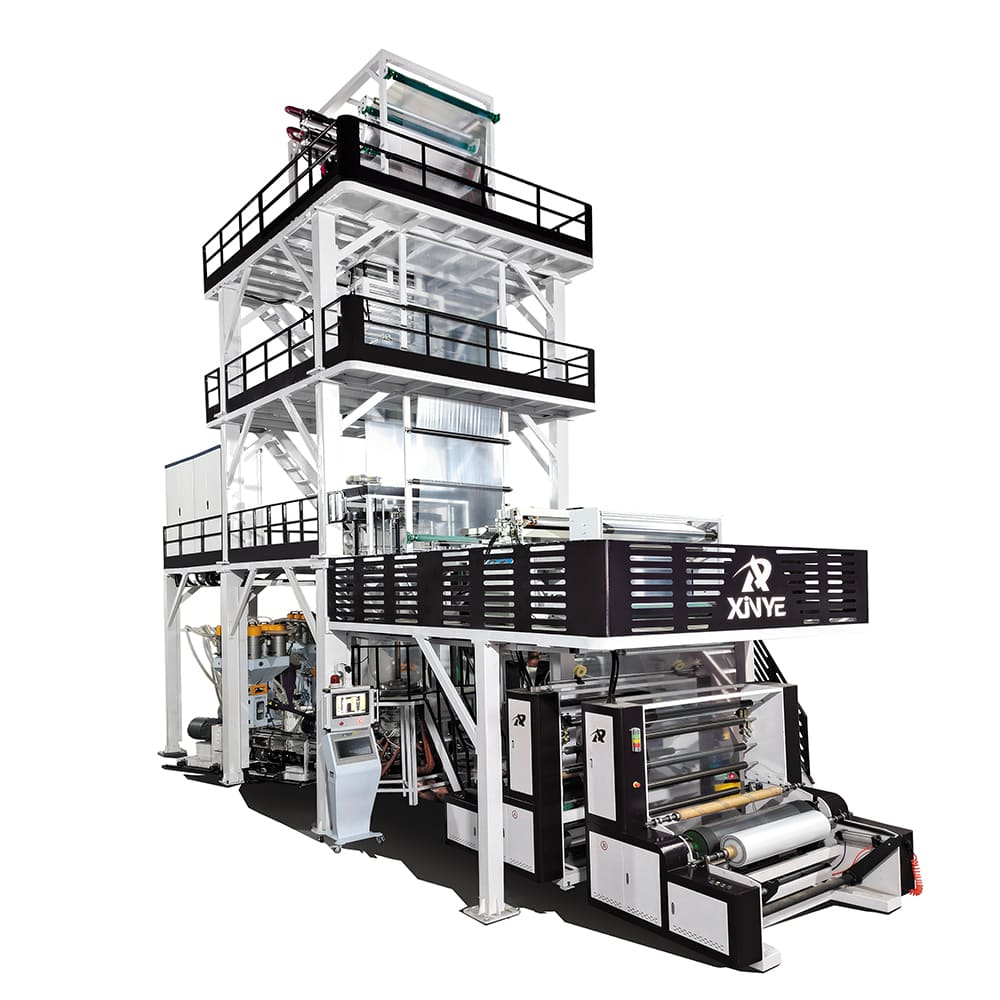
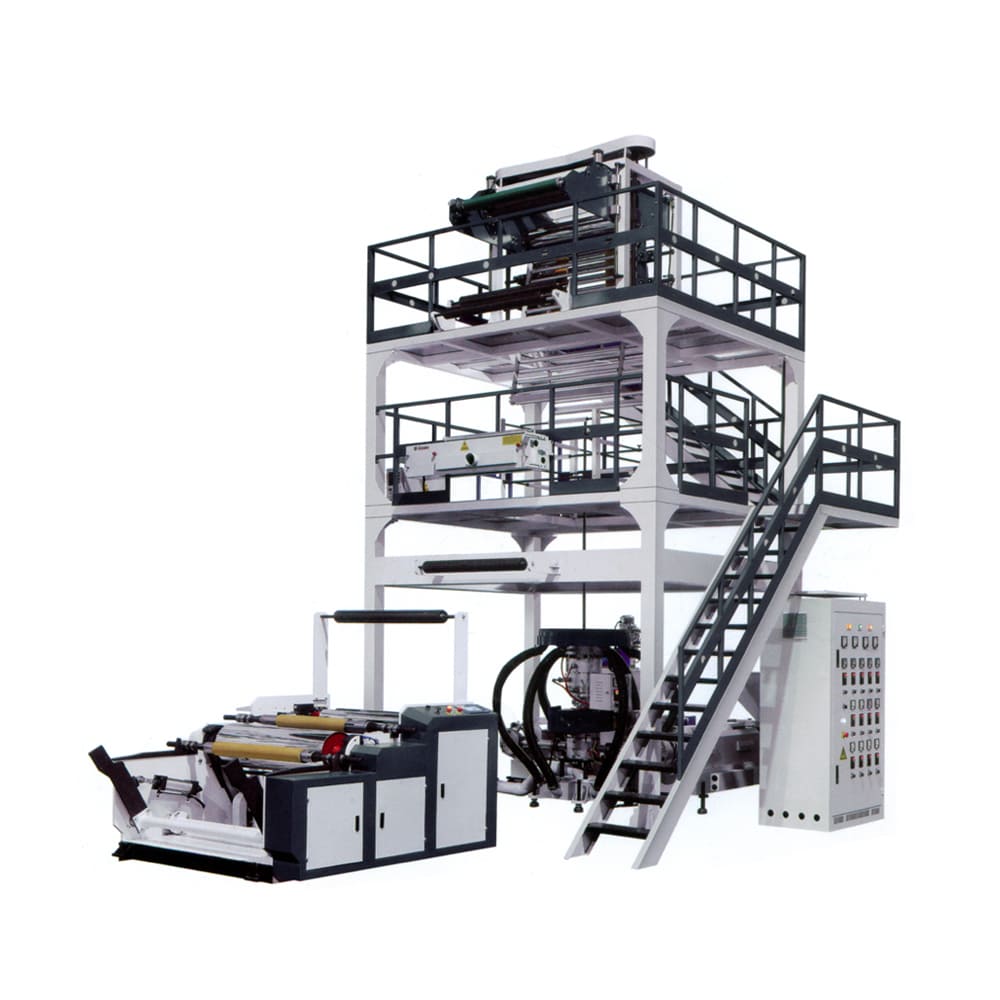
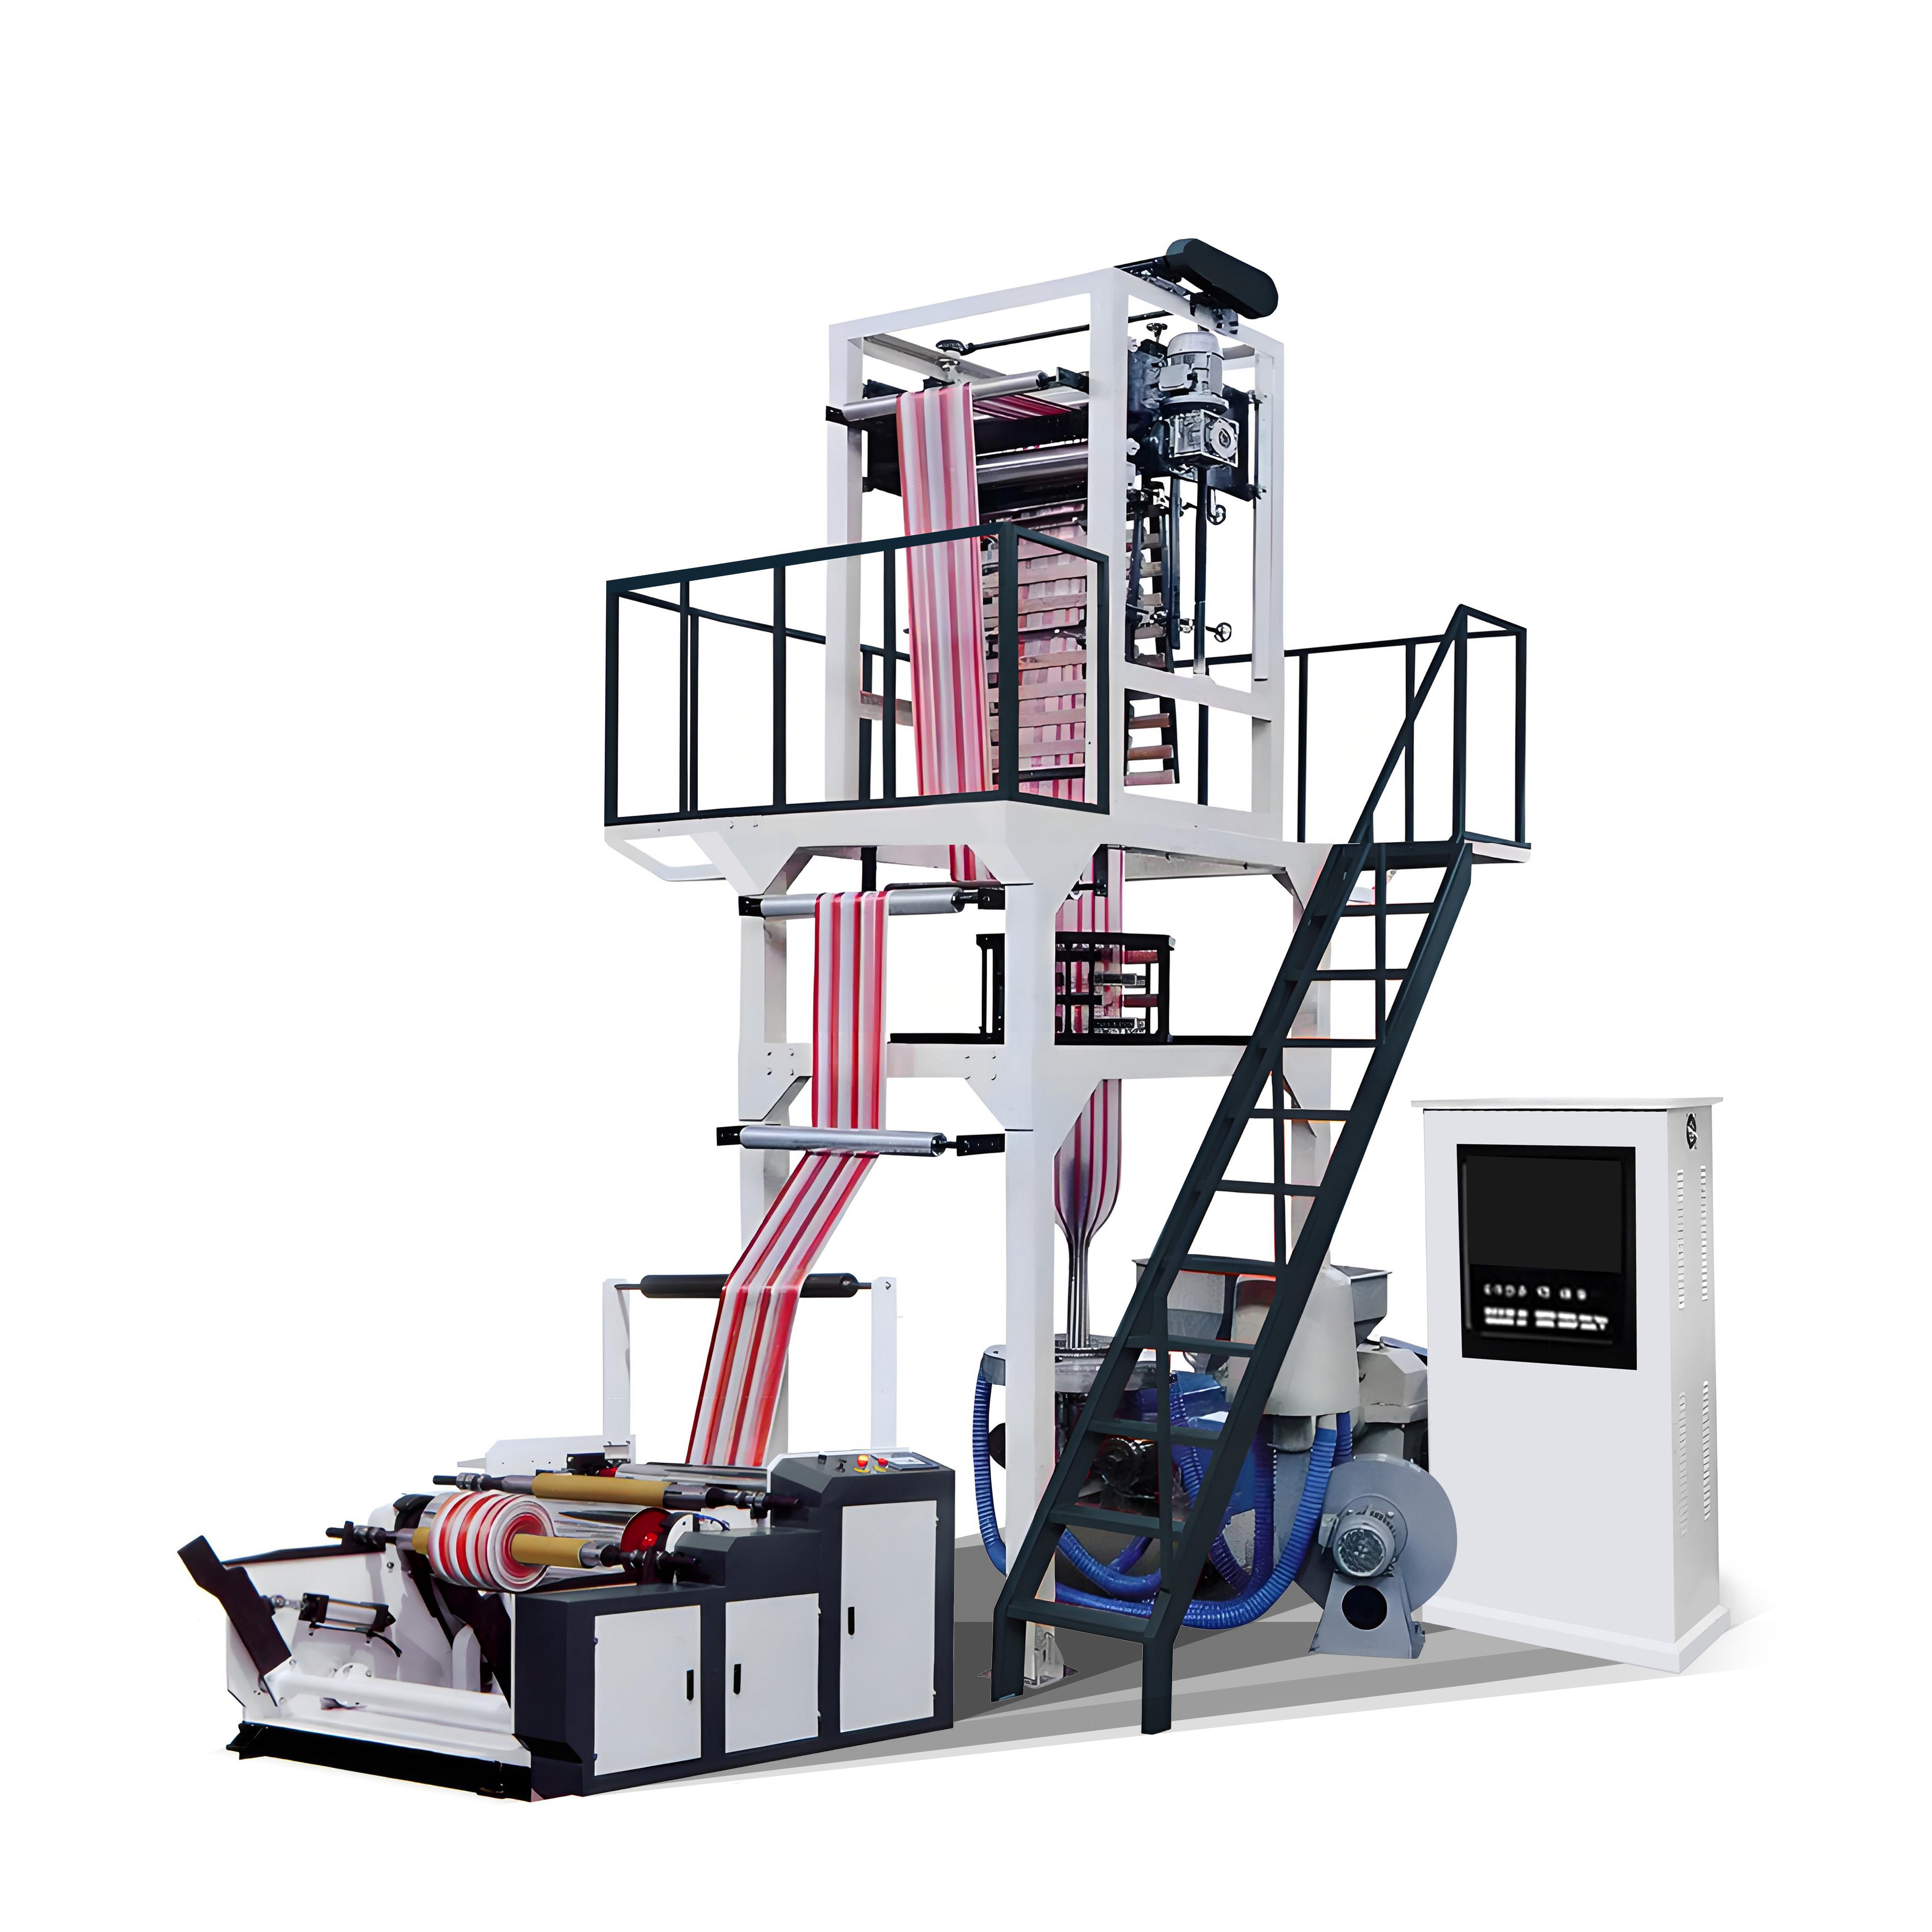
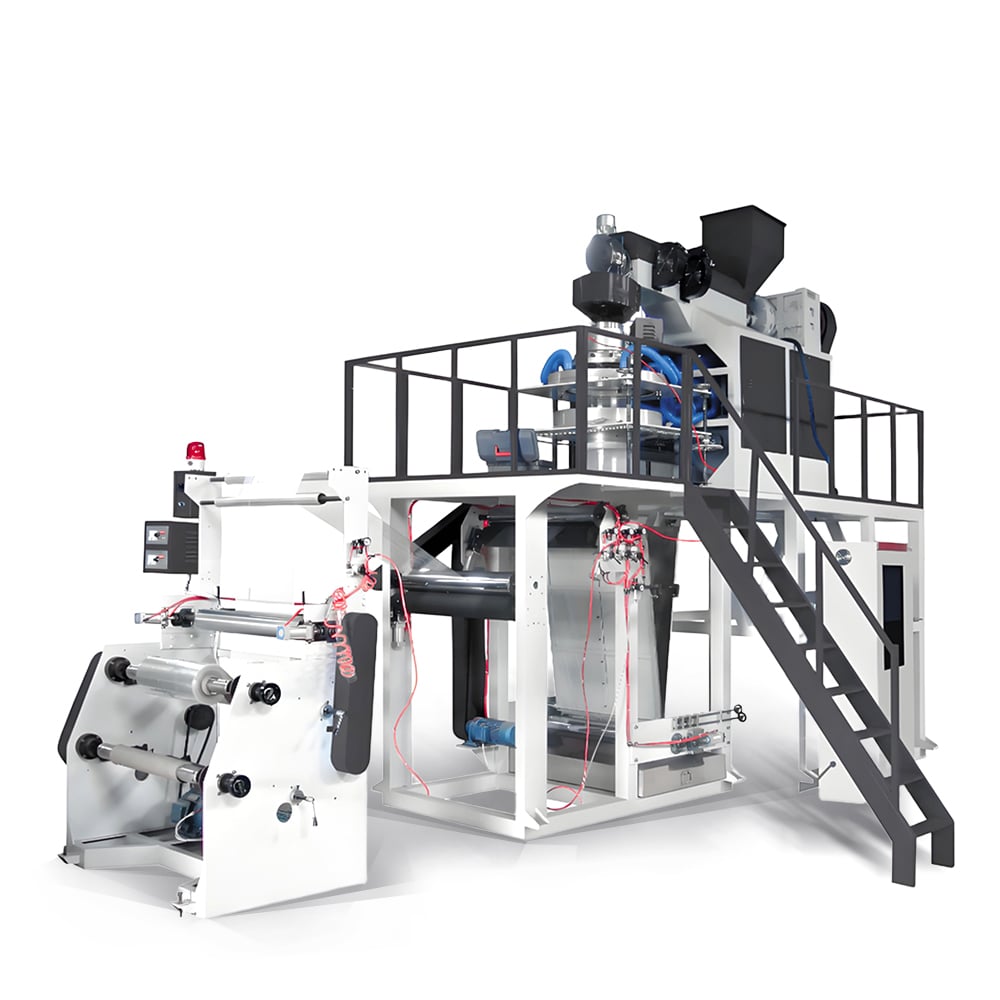
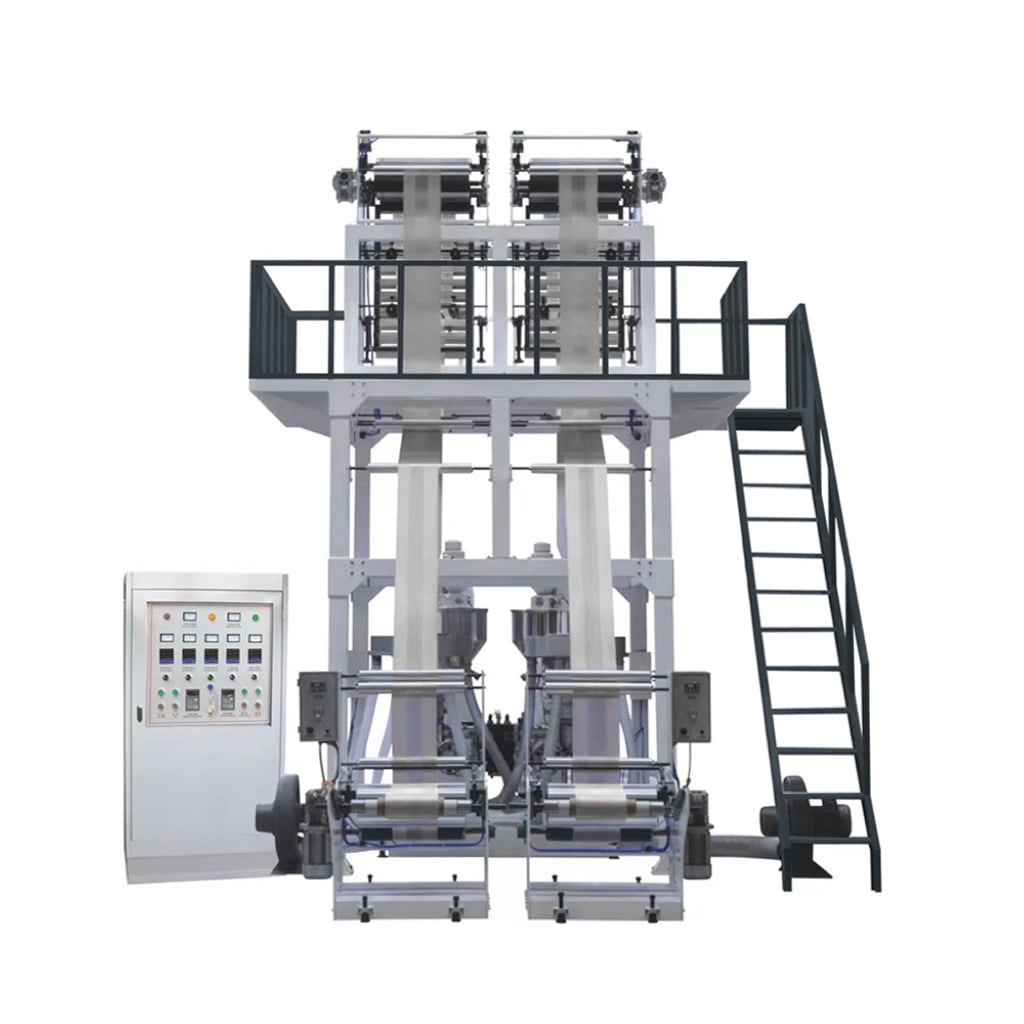
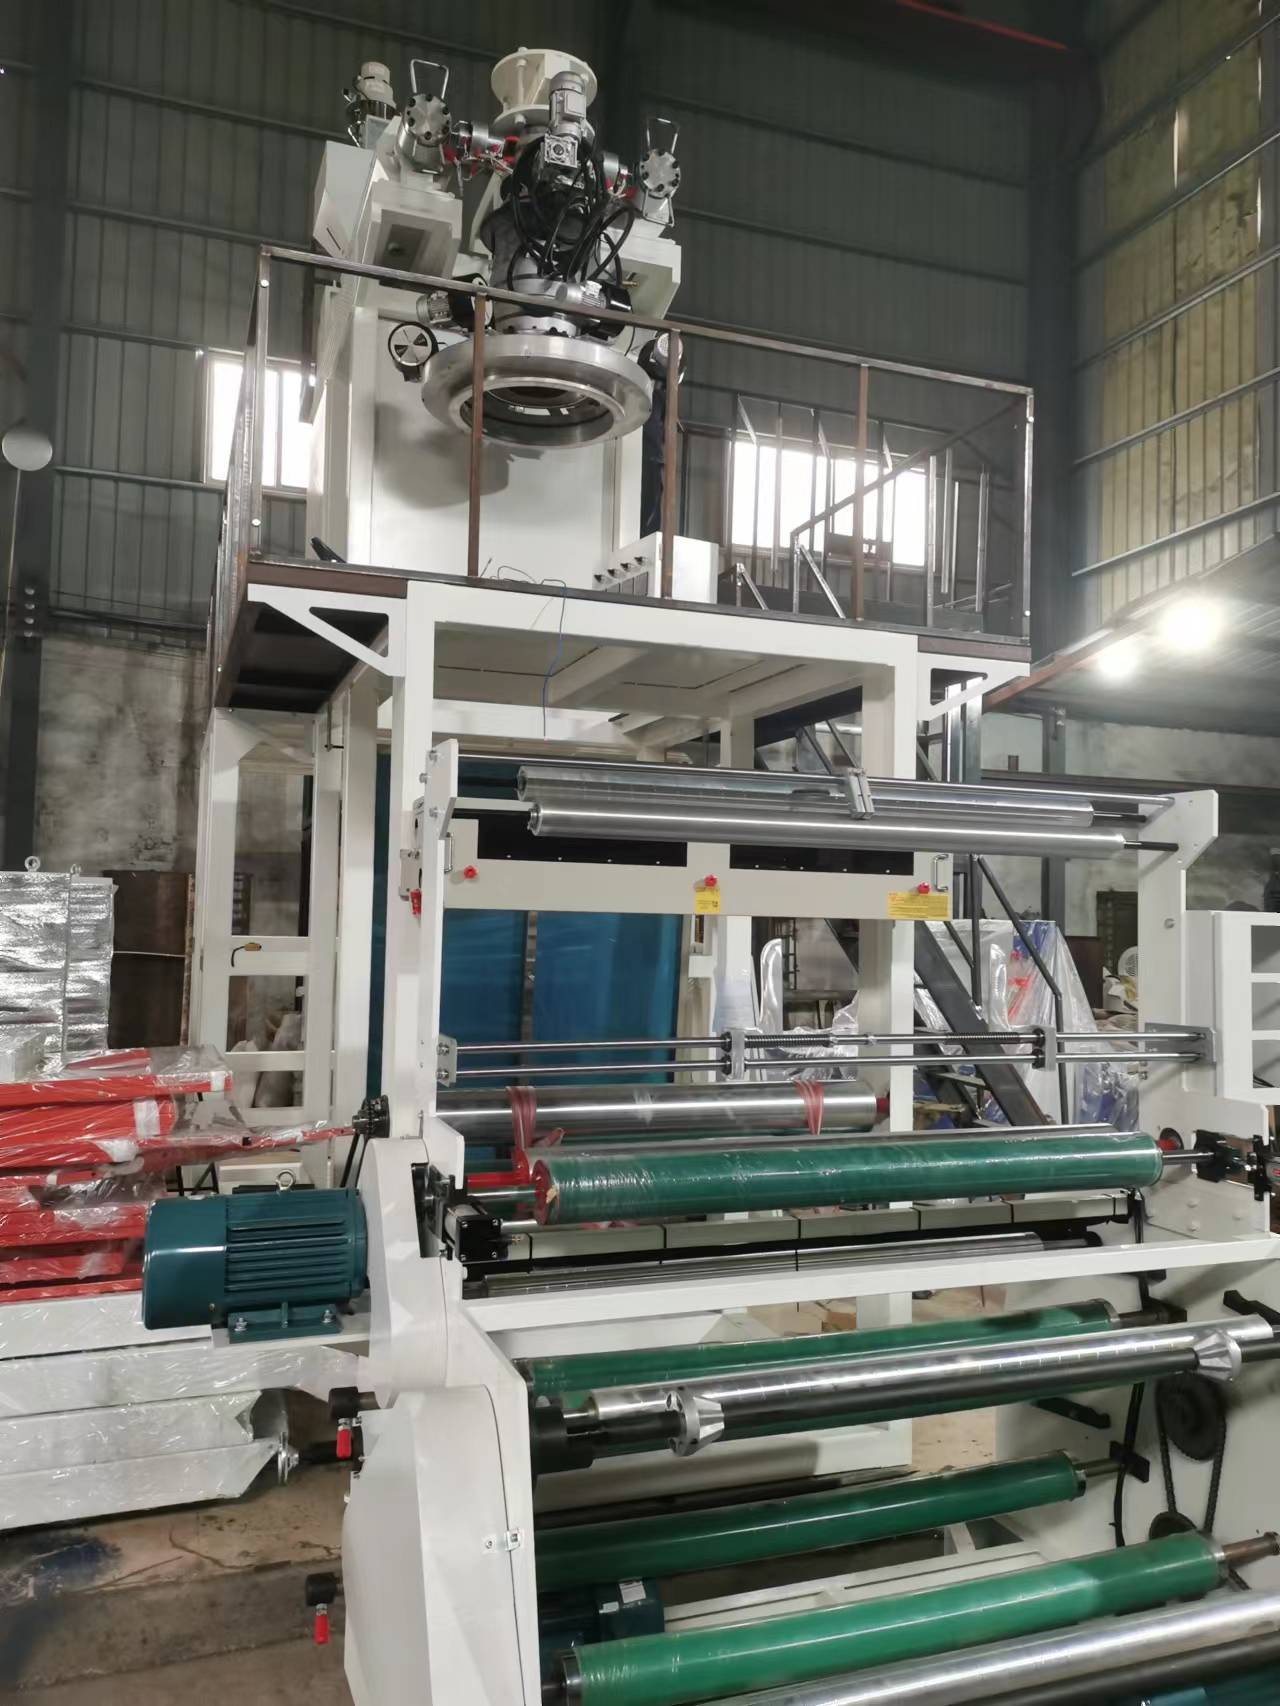
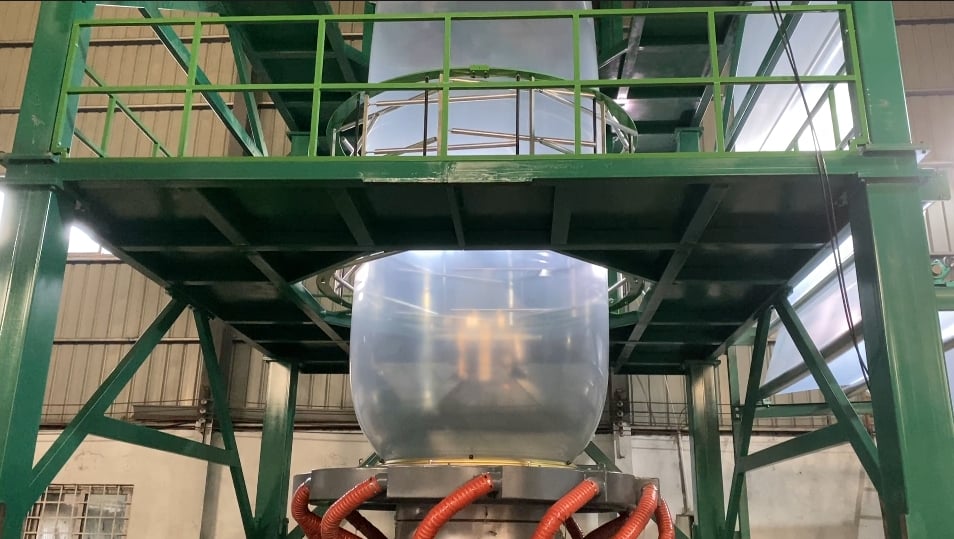
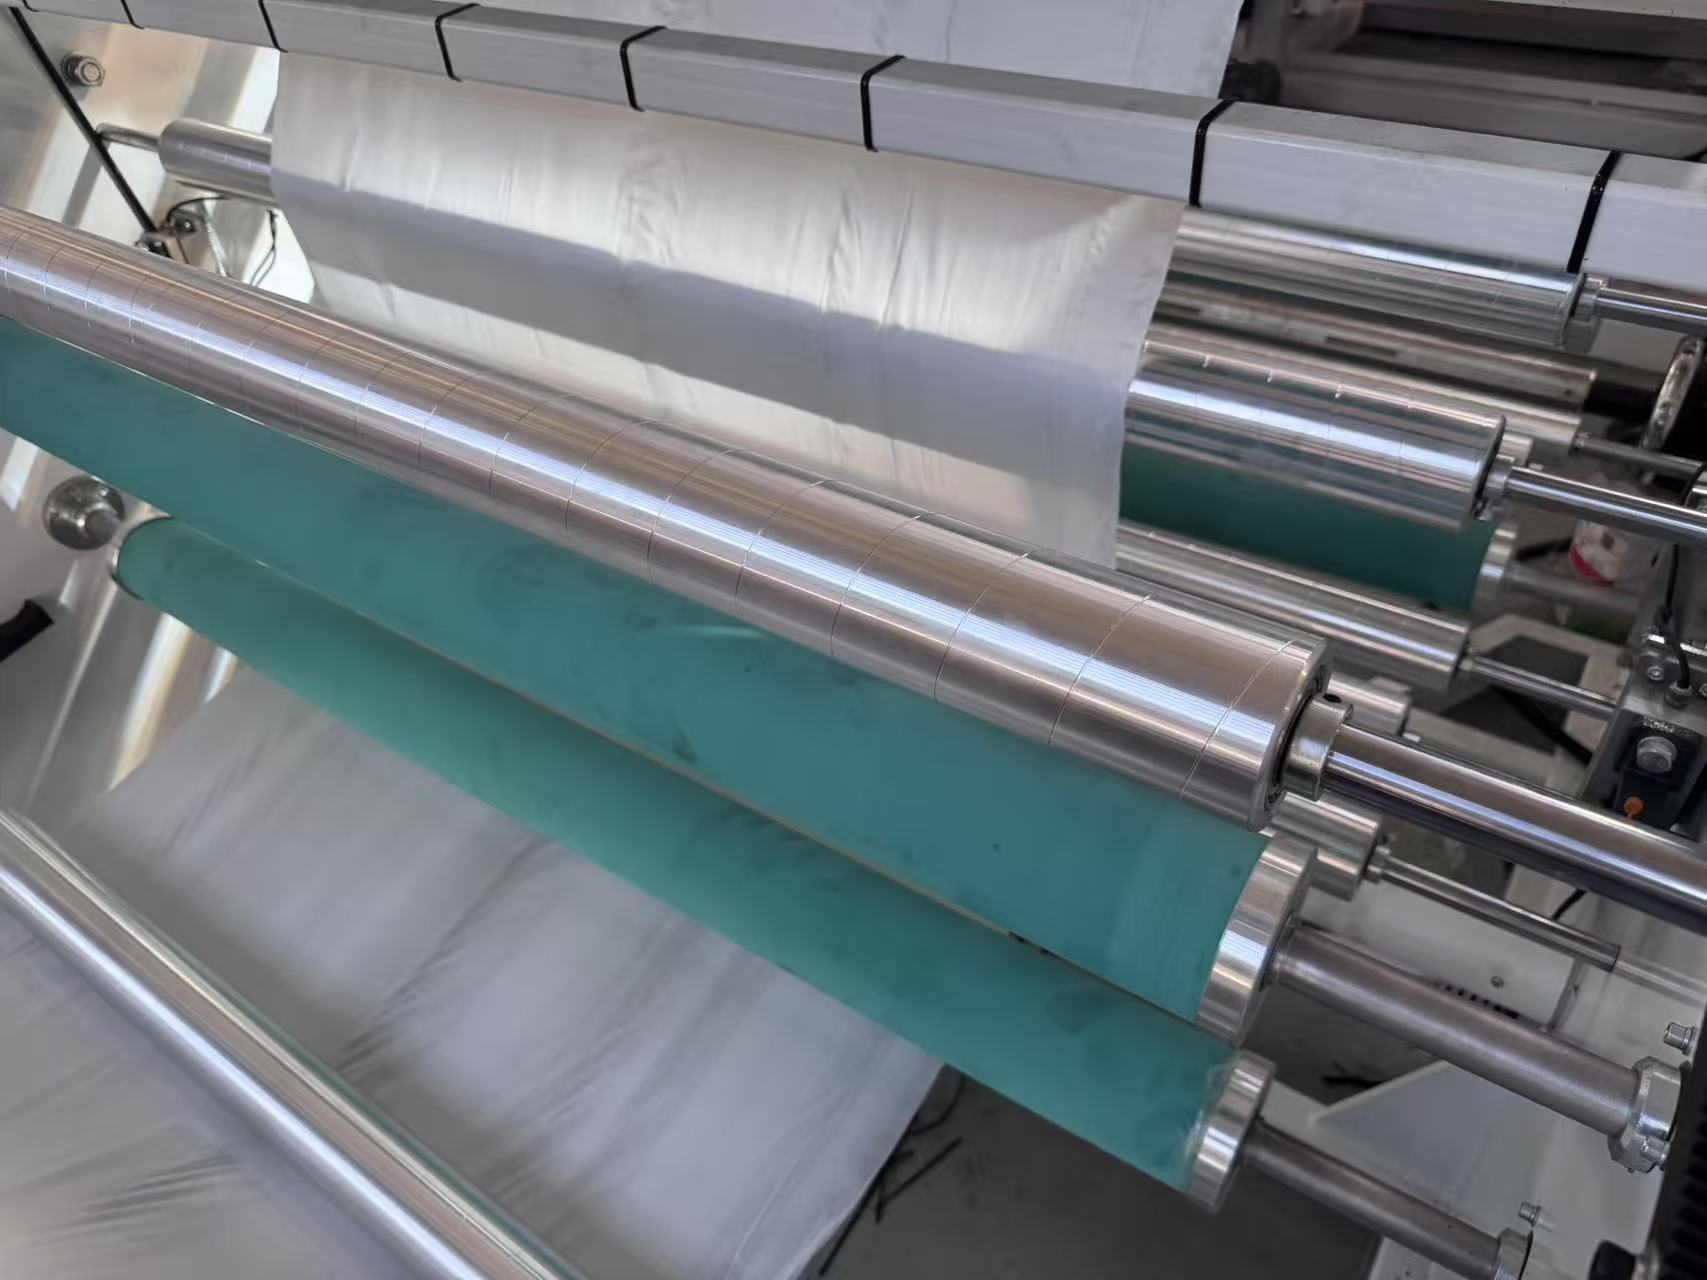
Blown polyethylene film represents a versatile packaging material manufactured through an extrusion process that creates thin, flexible plastic sheets with exceptional strength and durability. The blown polyethylene film production involves melting polyethylene resin and extruding it through a circular die, where air is introduced to inflate the film into a bubble. This innovative manufacturing technique allows blown polyethylene film to achieve superior mechanical properties compared to conventional cast films. The primary functions of blown polyethylene film include protecting products from moisture, oxygen, and physical damage during storage and transportation. The film's exceptional barrier properties make blown polyethylene film ideal for preserving food freshness, extending shelf life, and maintaining product integrity. Technologically, blown polyethylene film features enhanced puncture resistance, improved tear strength, and superior flexibility, making it perform reliably under demanding conditions. Key technological features of blown polyethylene film include multi-layer construction capabilities, enabling customized barrier performance for specific applications. The blown polyethylene film can be produced in various thicknesses and with specialized properties such as anti-static characteristics, UV protection, and enhanced slip resistance. Applications for blown polyethylene film span across food packaging, industrial wrapping, agricultural films, and protective coverings. The versatility of blown polyethylene film makes it the preferred choice for manufacturers seeking cost-effective, high-performance packaging solutions that deliver consistent quality and reliability.
New Products

Blown polyethylene film delivers exceptional value to customers through its outstanding combination of strength, flexibility, and cost-effectiveness. The primary advantage of choosing blown polyethylene film lies in its superior puncture and tear resistance, which protects your products during handling, storage, and transportation without compromising performance. Unlike inferior alternatives, blown polyethylene film maintains integrity even under extreme stress, reducing product loss and waste. Operationally, blown polyethylene film offers significant benefits through its ease of use and compatibility with standard packaging equipment. You can integrate blown polyethylene film seamlessly into existing production lines without requiring expensive modifications or specialized machinery. The lightweight nature of blown polyethylene film reduces shipping costs and environmental impact, directly improving your bottom line while supporting sustainability goals. For specific applications, blown polyethylene film excels in food packaging, industrial protection, and agricultural uses. The material's moisture barrier properties ensure products remain fresh longer, extending shelf life and reducing spoilage. Blown polyethylene film also provides excellent clarity and printability, enabling attractive product presentation and brand visibility on retail shelves. Decision-useful context shows that blown polyethylene film delivers superior performance-to-cost ratios compared to alternative materials. By choosing blown polyethylene film, businesses achieve reliable product protection while maintaining competitive pricing. The durability of blown polyethylene film means fewer packaging failures, reduced returns, and enhanced customer satisfaction. Additionally, blown polyethylene film supports regulatory compliance in food and pharmaceutical applications, providing peace of mind and protecting your brand reputation. Its versatility allows customization for specific needs, ensuring you receive exactly the protective solution your products require.

Tips And Tricks

How Multi-Layer Film Blowing Technology Improves Packaging Film Performance

31

Jan

How Multi-Layer Film Blowing Technology Improves Packaging Film Performance

Barrier Performance Optimization Through Strategic Layer Design Oxygen and Moisture Barrier Gains in 5- vs. 7-Layer Configurations How layers are arranged in packaging materials really affects how well they block out unwanted elements. According to...
View More
Why Biodegradable Film Blowing Machines Are Gaining Global Attention

31

Jan

Why Biodegradable Film Blowing Machines Are Gaining Global Attention

Global Demand Surge Driven by Regulation, ESG, and Market Readiness EU Plastic Strategy, U.S. State Bans, and APAC Policy Acceleration Regulations around the globe are pushing companies toward biodegradable film blowing machines at an impressive pa...
View More
Twin Head vs Single Head Film Blowing Machines: Production Strategy Insights

31

Jan

Twin Head vs Single Head Film Blowing Machines: Production Strategy Insights

Production Capacity and Operational Efficiency: Twin Head vs Single Head Film Blowing Machines Throughput, Line Speed, and Uptime: Quantifying Real-World Output Gains Twin head film blowing machines typically produce about 30 to 50 percent more mat...
View More
Control Panel Design in Automated Film Blowing Equipment

25

Feb

Control Panel Design in Automated Film Blowing Equipment

Core HMI Design Principles for Operator Efficiency in Automated Film Blowing Equipment Ergonomic touch-screen layout and intuitive navigation for rapid parameter adjustment Good HMI design begins with touch screens that are easy on the eyes and ha...
View More

Let Us Help You with Pricing

Our sales team will contact you shortly with pricing details and suggestions.
Name
Company Name
Email
Mobile
Message
0/1000

blown polyethylene film

Superior Puncture and Tear Resistance

Superior Puncture and Tear Resistance

The exceptional puncture and tear resistance of blown polyethylene film sets it apart from competing packaging materials in the market. This critical advantage directly impacts product protection during the entire supply chain journey from manufacturing through final delivery. Blown polyethylene film maintains structural integrity even when exposed to sharp objects, rough handling, and environmental stressors that would compromise weaker films. The molecular structure of blown polyethylene film creates a resilient barrier that absorbs impact energy, preventing catastrophic failures that lead to product damage and customer dissatisfaction. For businesses handling fragile or sensitive products, blown polyethylene film provides the confidence that packages will arrive intact and in perfect condition. This superior durability reduces return rates, minimizes warranty claims, and protects brand reputation. Industries ranging from electronics to fresh produce rely on blown polyethylene film specifically for its proven track record of safeguarding valuable merchandise. The long-term cost savings from reduced damage claims substantially exceed the minimal additional investment required for blown polyethylene film.
Exceptional Moisture and Oxygen Barrier Properties

Exceptional Moisture and Oxygen Barrier Properties

Blown polyethylene film creates a highly effective barrier against moisture intrusion and oxygen penetration, essential factors for maintaining product freshness and extending shelf life significantly. The protective properties of blown polyethylene film directly address the primary concerns of food manufacturers, pharmaceutical companies, and retailers seeking to preserve product quality. By utilizing blown polyethylene film, businesses prevent oxidation that degrades flavor, nutrients, and potency in sensitive products. The moisture resistance of blown polyethylene film protects contents from humidity-related deterioration, mold formation, and spoilage that render products unmarketable. This barrier capability of blown polyethylene film is particularly valuable for moisture-sensitive applications including dried goods, electronics, and pharmaceuticals requiring extended shelf life. The breathability characteristics of blown polyethylene film can be customized to meet specific oxygen transmission requirements for different product categories. Food producers utilizing blown polyethylene film consistently report extended shelf life, reduced waste, and improved customer satisfaction. The reliable barrier performance of blown polyethylene film enables businesses to confidently ship products globally without compromising quality or safety standards.
Cost-Effective Manufacturing and Easy Integration

Cost-Effective Manufacturing and Easy Integration

Blown polyethylene film provides remarkable cost advantages through efficient manufacturing processes and seamless integration with existing production infrastructure. Businesses implementing blown polyethylene film experience minimal disruption to current operations since the material works compatibly with standard packaging equipment and machinery. The economic efficiency of blown polyethylene film stems from its lightweight nature, reducing material waste and transportation expenses significantly. Manufacturers appreciate how blown polyethylene film can be produced in various thicknesses and specifications without requiring expensive custom equipment investments. The procurement cost of blown polyethylene film remains competitive compared to premium alternatives while delivering superior performance characteristics. Implementation of blown polyethylene film eliminates costly equipment upgrades, retraining requirements, and operational downtime associated with transitioning to incompatible materials. The standardization of blown polyethylene film across industry applications means abundant supplier options, fostering competitive pricing and reliable availability. Companies prioritizing profitability and operational efficiency find blown polyethylene film represents the optimal balance between performance quality and economical investment, directly enhancing profitability margins.