IBC Blown Film: Superior Bulk Packaging

Let Us Help You with Pricing

Our sales team will contact you shortly with pricing details and suggestions.
Name
Company Name
Email
Mobile
Message
0/1000

ibc blown film

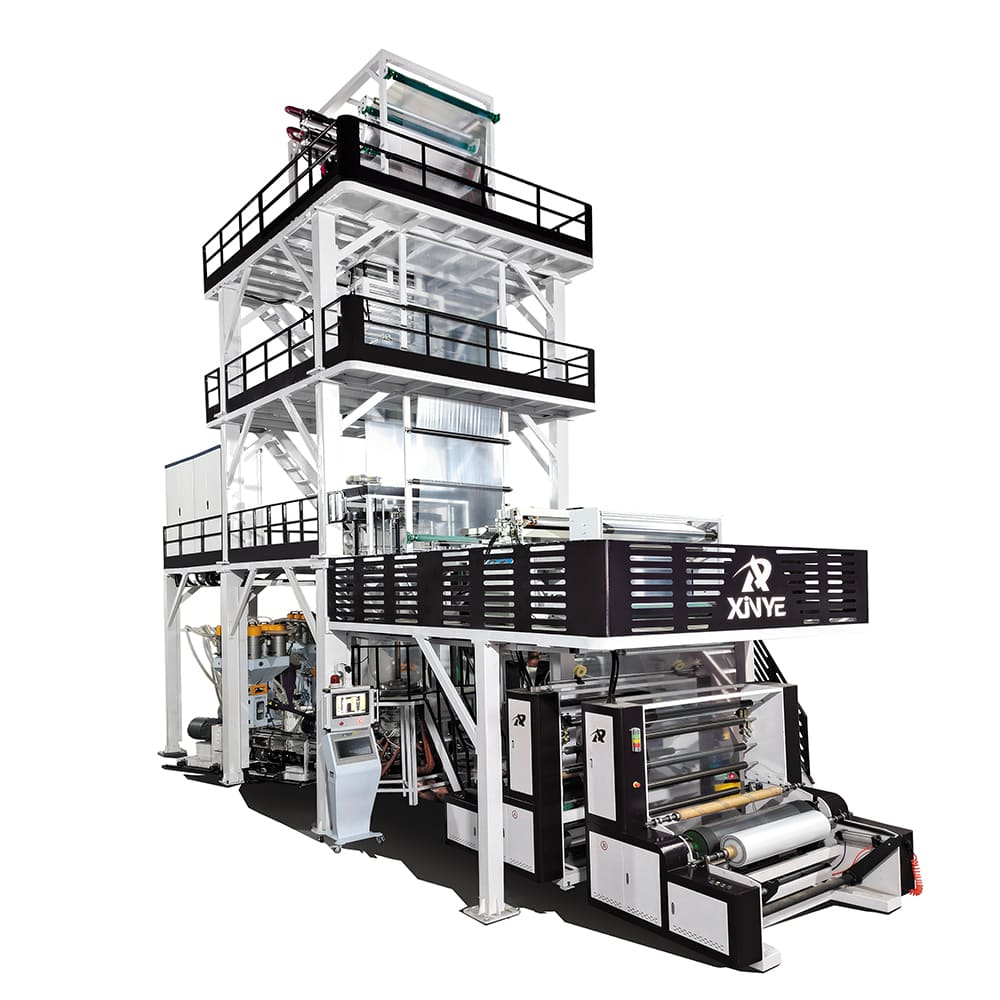
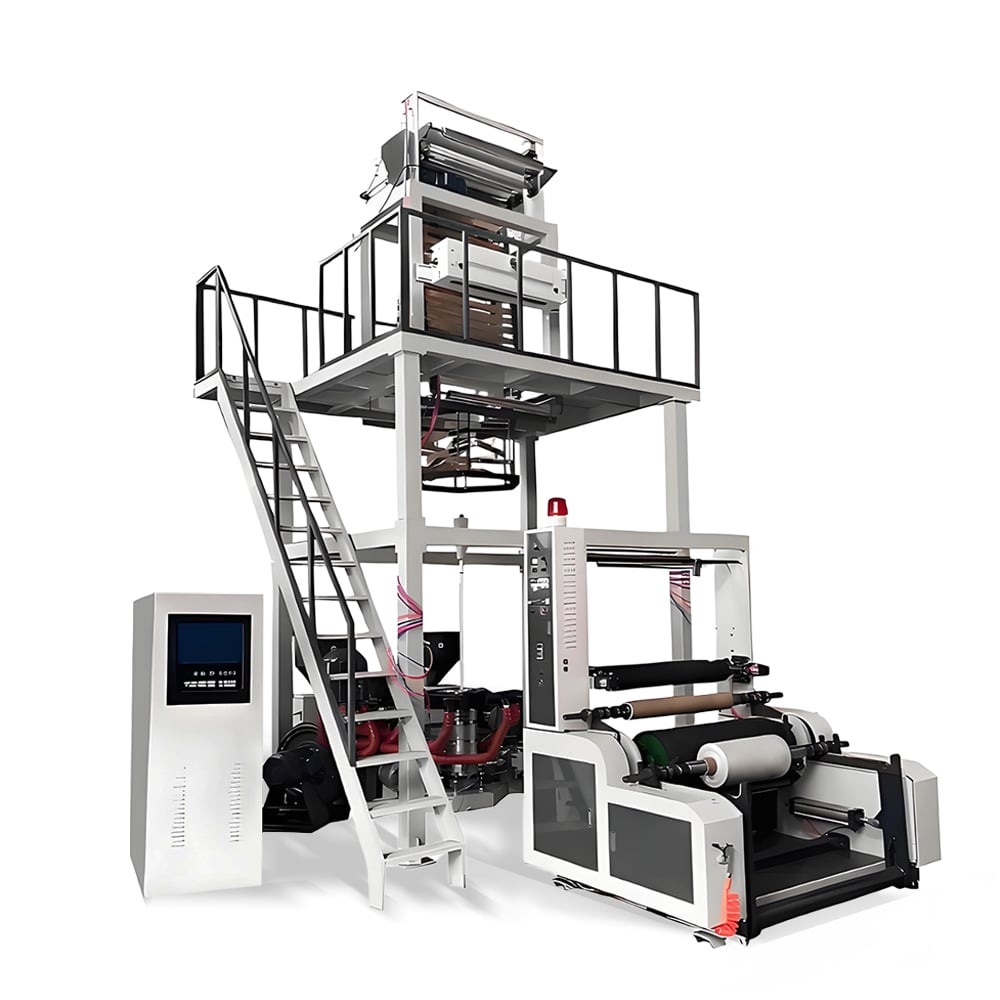
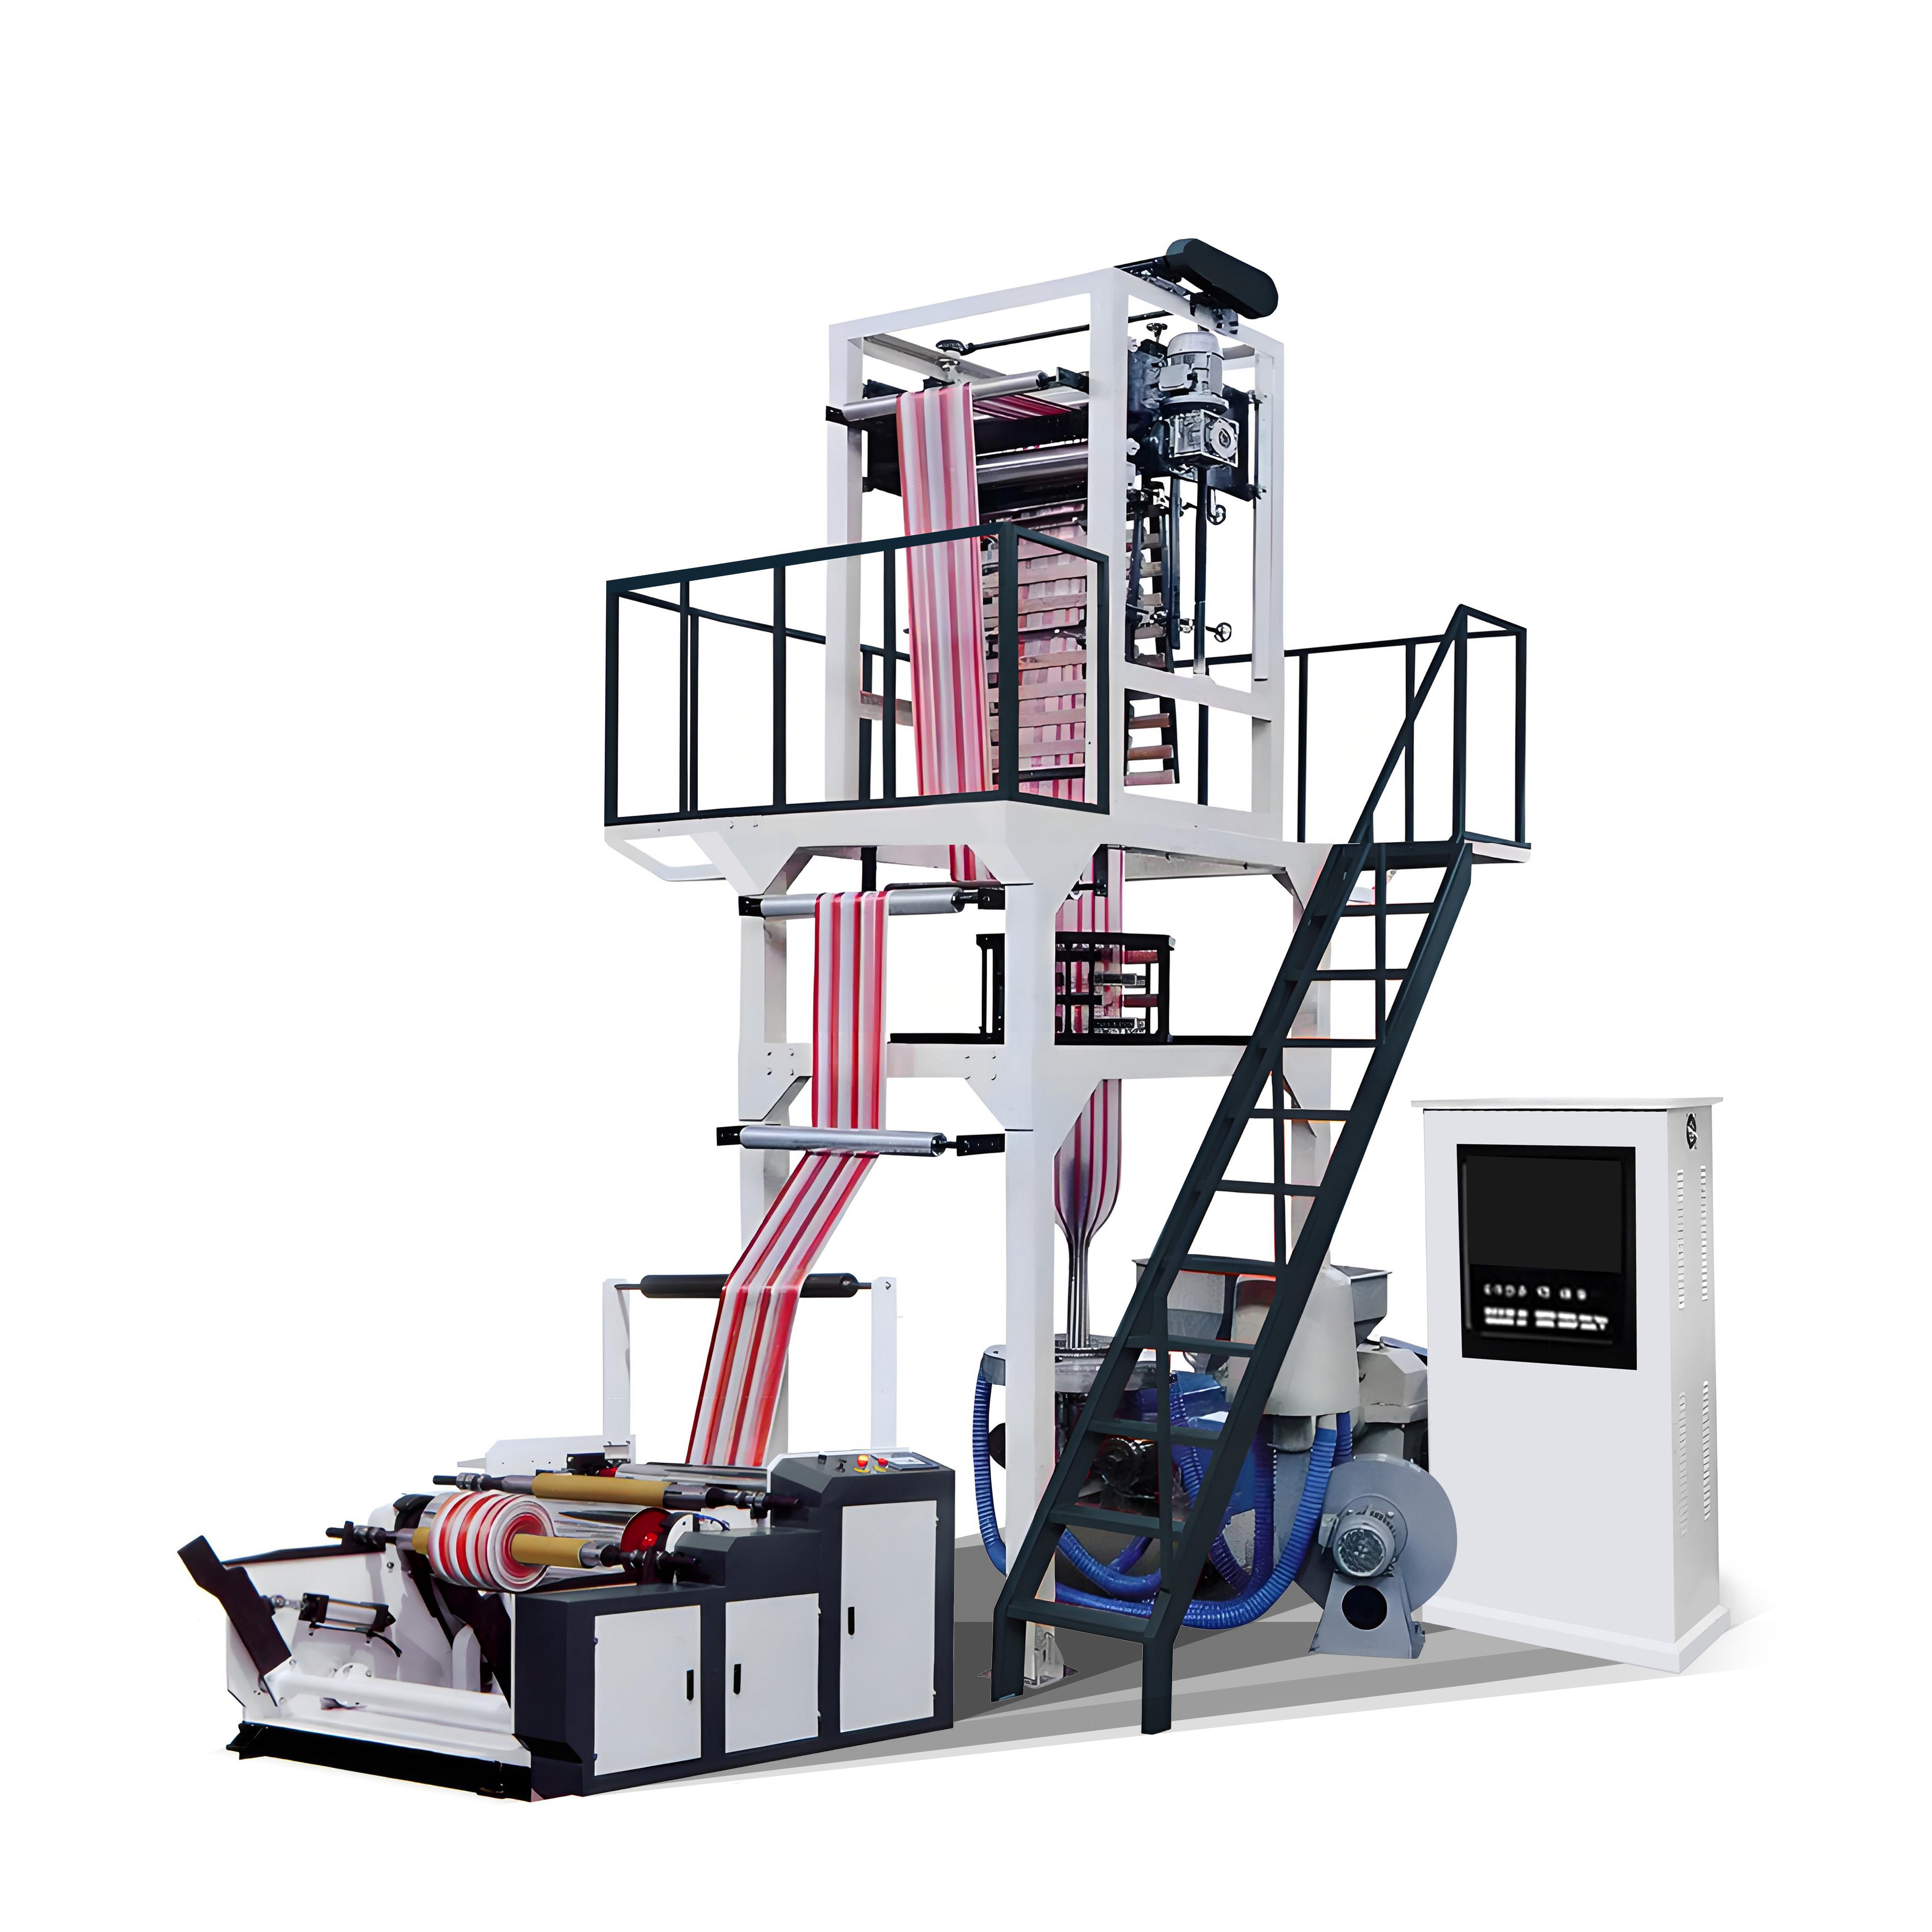
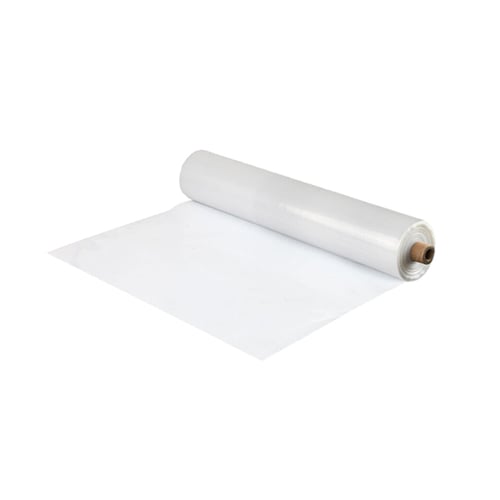
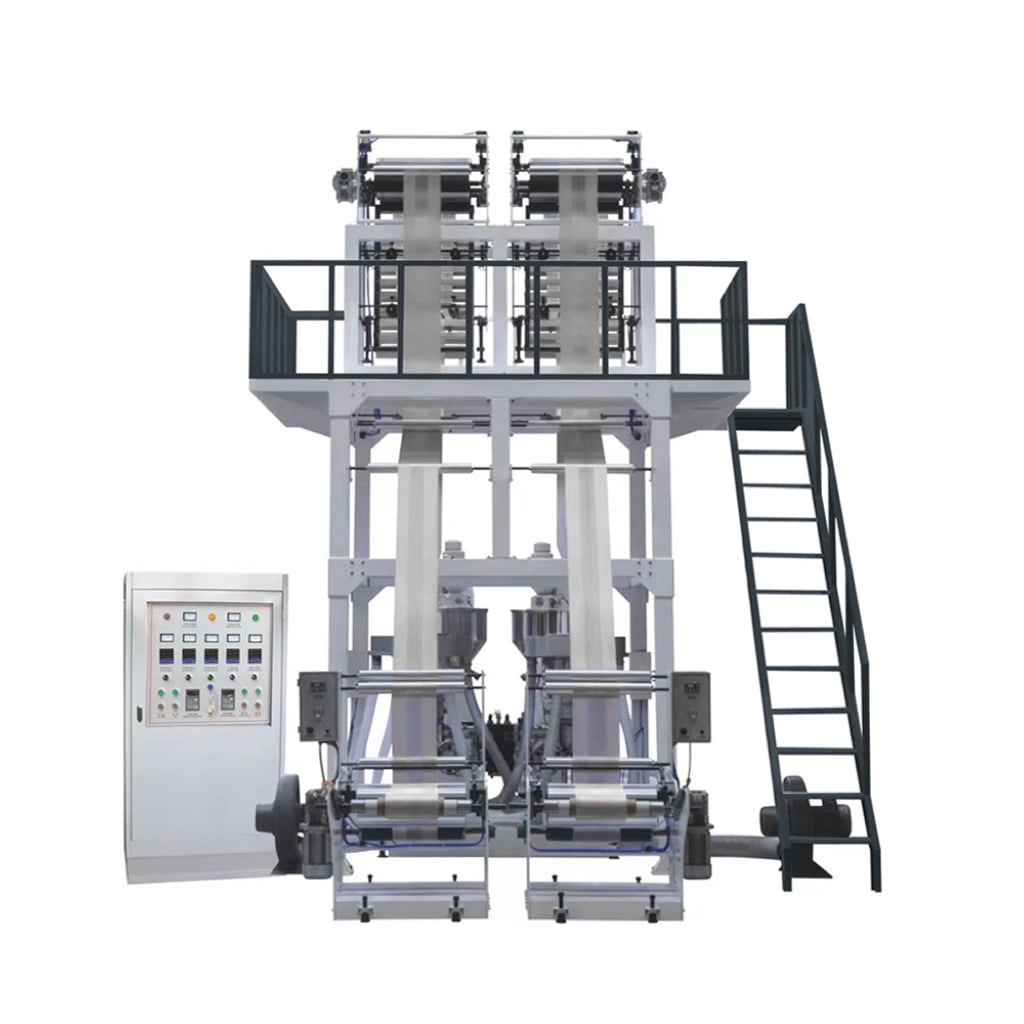
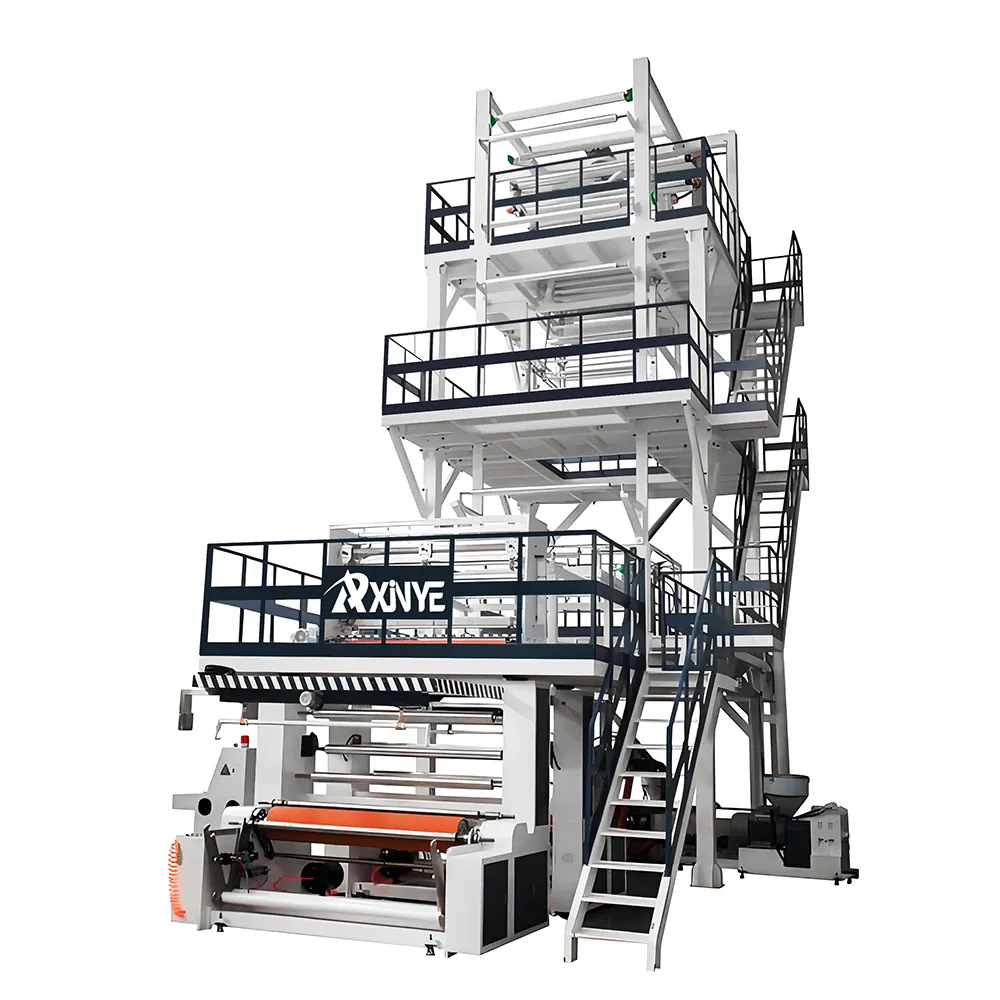
IBC blown film represents a cutting-edge packaging solution designed specifically for intermediate bulk container applications. This specialized film technology delivers exceptional performance characteristics that make it ideal for storing and transporting various industrial liquids and granular materials. IBC blown film is manufactured using advanced extrusion processes that create uniform, multi-layered structures with superior strength properties. The primary functions of IBC blown film include providing robust containment, protecting product integrity during storage and transit, and ensuring environmental safety through reliable barrier properties. The technological features of IBC blown film incorporate high-density polyethylene and specialized resin blends that withstand extreme pressure conditions and temperature fluctuations. These films demonstrate remarkable puncture resistance and tear strength, critical attributes for demanding industrial environments. IBC blown film applications span across numerous industries, including chemical manufacturing, food processing, pharmaceutical distribution, and agricultural sectors. The versatility of IBC blown film makes it suitable for both hazardous and non-hazardous material containment. Modern IBC blown film production employs precision control systems that ensure consistent thickness distribution and minimal defects throughout the manufacturing process. The film's exceptional durability and reliability have established it as the preferred choice for companies requiring dependable bulk packaging solutions that meet stringent international standards and regulatory requirements.

Popular Products

IBC blown film offers substantial practical benefits that directly address the needs of businesses requiring dependable bulk packaging solutions. The primary advantage lies in its exceptional durability, as IBC blown film provides outstanding resistance to punctures, tears, and environmental stress cracking. This enhanced durability significantly reduces product loss, contamination risks, and costly replacement expenses associated with packaging failures. From an operational perspective, IBC blown film delivers remarkable cost efficiency by extending container lifespan and minimizing waste. Businesses benefit from reduced material consumption while maintaining superior protective capabilities. The lightweight nature of IBC blown film facilitates easier handling, storage, and transportation, thereby lowering operational labor costs and energy requirements throughout the supply chain. IBC blown film excels in application suitability across diverse industrial sectors, including chemical storage, food distribution, pharmaceutical packaging, and agricultural transport. The film's versatile composition accommodates various material types, from aggressive chemicals to sensitive food products, without compromising containment integrity or product quality. Decision-useful product context demonstrates that IBC blown film complies with international packaging standards and regulatory frameworks, providing businesses with confidence and legal certainty. The film's superior barrier properties protect contents from moisture, oxygen, and external contaminants, ensuring product freshness and efficacy throughout extended storage periods. Companies choosing IBC blown film gain competitive advantages through improved supply chain efficiency, enhanced product protection, and demonstrated commitment to sustainable, reliable packaging practices that resonate with environmentally conscious customers and regulatory bodies.

Practical Tips

How Multi-Layer Film Blowing Technology Improves Packaging Film Performance

31

Jan

How Multi-Layer Film Blowing Technology Improves Packaging Film Performance

Barrier Performance Optimization Through Strategic Layer Design Oxygen and Moisture Barrier Gains in 5- vs. 7-Layer Configurations How layers are arranged in packaging materials really affects how well they block out unwanted elements. According to...
View More
The Role of Film Thickness Control in High-Quality Blown Film Production

31

Jan

The Role of Film Thickness Control in High-Quality Blown Film Production

Why Film Thickness Control Is Fundamental to Blown Film Quality How thickness uniformity directly determines mechanical strength, optical clarity, and barrier performance Getting film thickness just right matters a lot for blown film quality becaus...
View More
Twin Head vs Single Head Film Blowing Machines: Production Strategy Insights

31

Jan

Twin Head vs Single Head Film Blowing Machines: Production Strategy Insights

Production Capacity and Operational Efficiency: Twin Head vs Single Head Film Blowing Machines Throughput, Line Speed, and Uptime: Quantifying Real-World Output Gains Twin head film blowing machines typically produce about 30 to 50 percent more mat...
View More
How Automatic Thickness Control Systems Work in Film Blowing Machines

25

Feb

How Automatic Thickness Control Systems Work in Film Blowing Machines

Core Principle of Film Blowing Machines: Closed-Loop Feedback for Real-Time Thickness Correction At the heart of precision in film blowing machines lies the closed-loop feedback system—a dynamic process where thickness measurements directly ...
View More

Let Us Help You with Pricing

Our sales team will contact you shortly with pricing details and suggestions.
Name
Company Name
Email
Mobile
Message
0/1000

ibc blown film

Superior Puncture and Tear Resistance

Superior Puncture and Tear Resistance

IBC blown film delivers exceptional puncture and tear resistance that sets it apart from conventional packaging materials. This critical feature stems from the film's sophisticated multi-layer construction and high-quality resin composition. When materials encounter rough handling, sharp edges, or abrasive surfaces during transportation and storage, IBC blown film maintains its structural integrity, preventing catastrophic failures that could compromise entire shipments. The enhanced resistance characteristics of IBC blown film directly translate to reduced product loss, minimized liability exposure, and improved customer satisfaction. Industries transporting hazardous materials particularly value this protective capability, as IBC blown film ensures regulatory compliance and worker safety. The durability advantage of IBC blown film means containers remain reliable throughout extended use cycles, delivering exceptional value for investment. Businesses experience fewer unexpected packaging failures, emergency replacements, and associated operational disruptions when relying on IBC blown film technology.
Exceptional Environmental and Chemical Barrier Protection

Exceptional Environmental and Chemical Barrier Protection

IBC blown film provides outstanding barrier properties that protect valuable contents from environmental degradation and chemical interaction. The specialized formulation of IBC blown film creates an effective seal against moisture penetration, oxygen exposure, and atmospheric contamination. This barrier functionality proves especially valuable for storing pharmaceutical products, specialty chemicals, and temperature-sensitive materials requiring precise environmental conditions. IBC blown film maintains product quality, potency, and efficacy throughout extended storage periods, ensuring goods reach end-users in optimal condition. The film's resistance to chemical permeation prevents unwanted interactions between packaging materials and contents, protecting both product integrity and packaging stability. Regulatory compliance becomes seamless when utilizing IBC blown film, as the material meets stringent international standards for food contact, pharmaceutical storage, and hazardous material containment. Companies leveraging IBC blown film gain competitive advantages through superior product preservation, reduced spoilage rates, and enhanced brand reputation for quality assurance.
Cost-Effective Durability and Extended Service Life

Cost-Effective Durability and Extended Service Life

IBC blown film delivers remarkable cost-effectiveness through its extended service life and outstanding durability characteristics. Unlike conventional packaging materials that require frequent replacement, IBC blown film containers withstand multiple use cycles while maintaining protective capabilities. This longevity directly reduces total cost of ownership by minimizing replacement frequency and associated procurement expenses. The strength-to-weight ratio of IBC blown film enables lighter packaging solutions that reduce transportation costs and carbon footprints without sacrificing protective performance. IBC blown film's resistance to degradation, cracking, and environmental stress ensures reliable performance across diverse climatic conditions and storage scenarios. Businesses implementing IBC blown film experience substantial operational savings through reduced waste generation, lower handling labor requirements, and optimized supply chain efficiency. The investment in quality IBC blown film packaging yields returns through improved product protection, decreased loss rates, and enhanced customer satisfaction. Companies strategically adopting IBC blown film strengthen their competitive positioning while demonstrating commitment to sustainable, economically prudent packaging practices.