Multilayer Blown Film | Advanced Packaging Solutions

Let Us Help You with Pricing

Our sales team will contact you shortly with pricing details and suggestions.
Name
Company Name
Email
Mobile
Message
0/1000

multilayer blown film

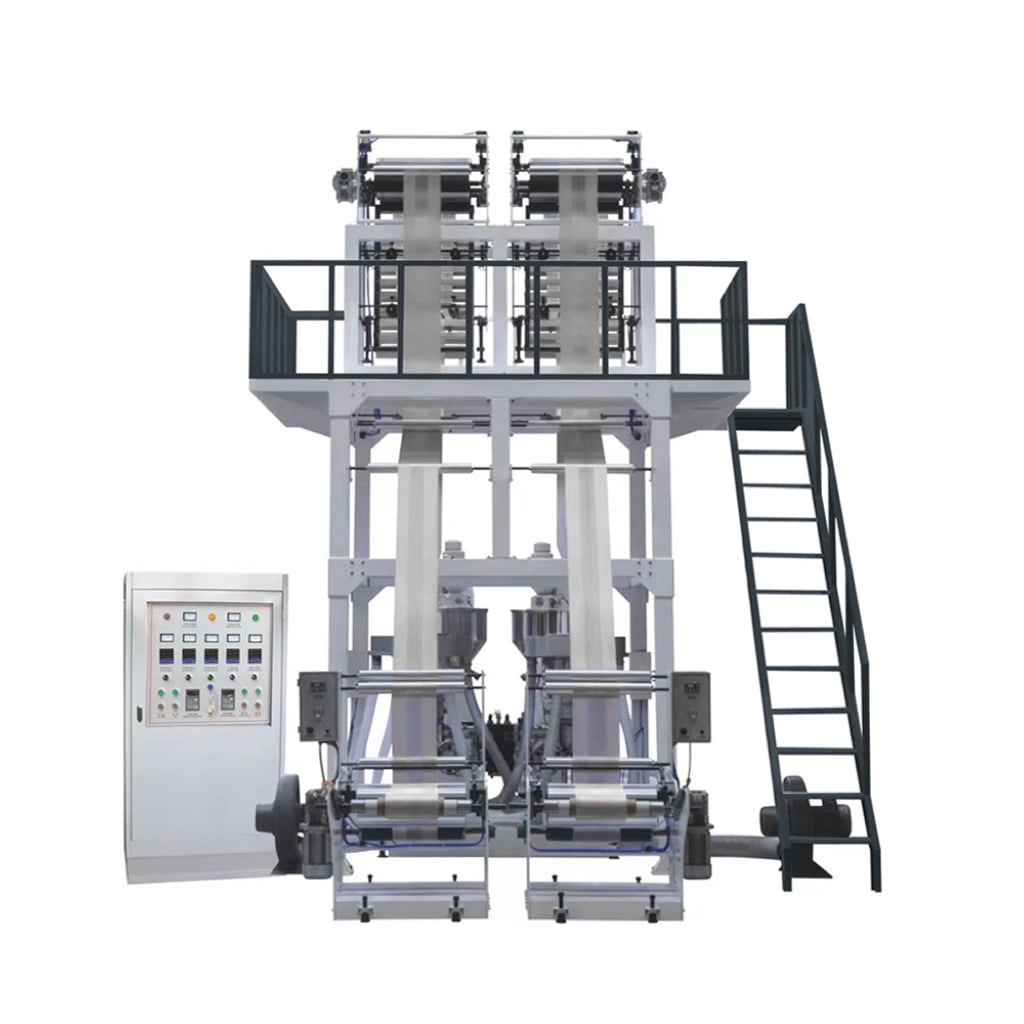
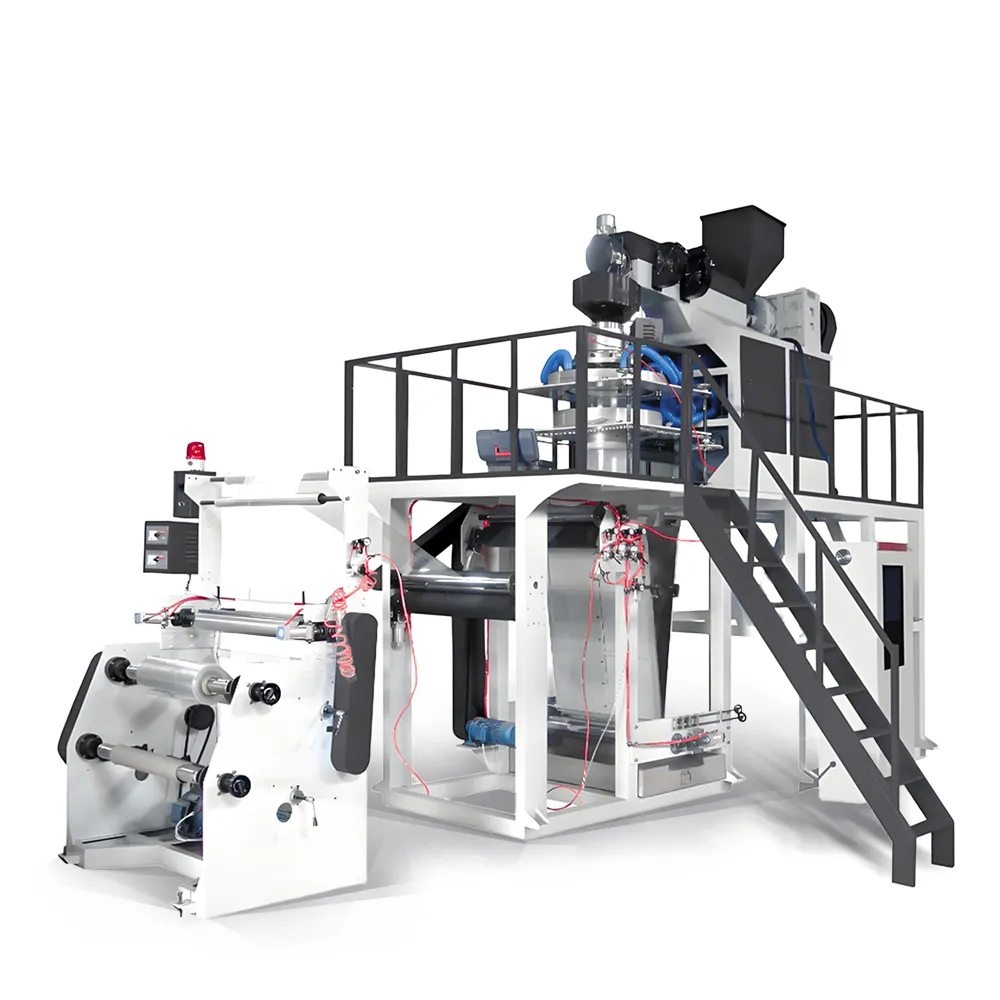
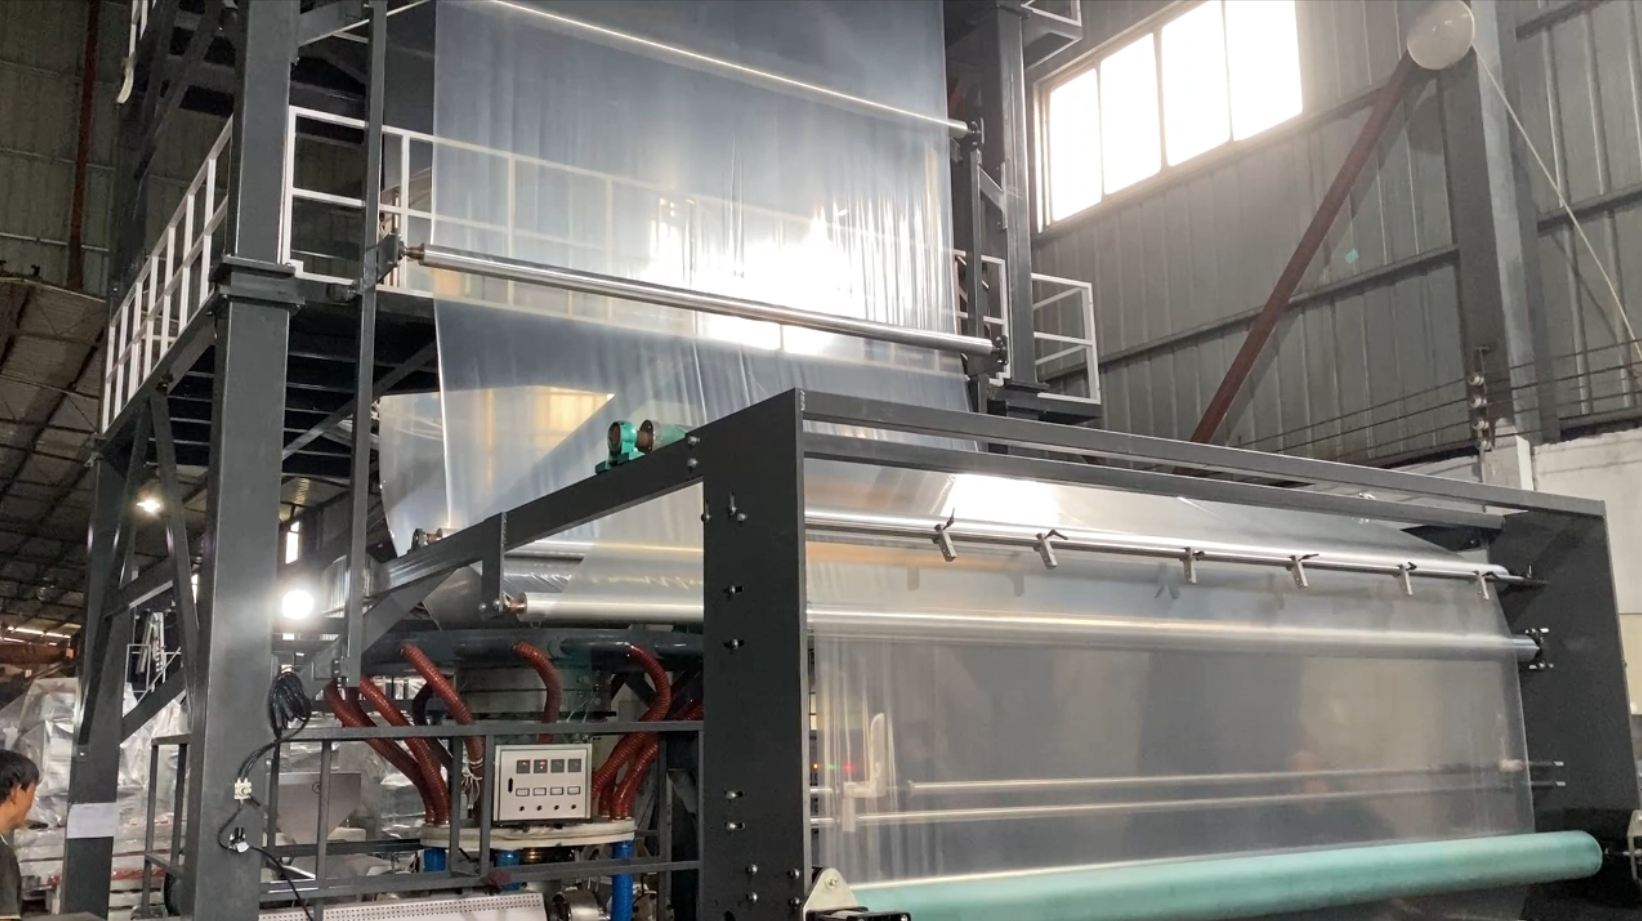
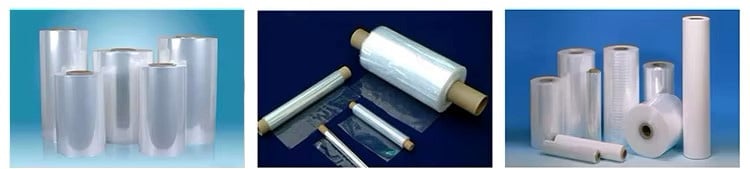
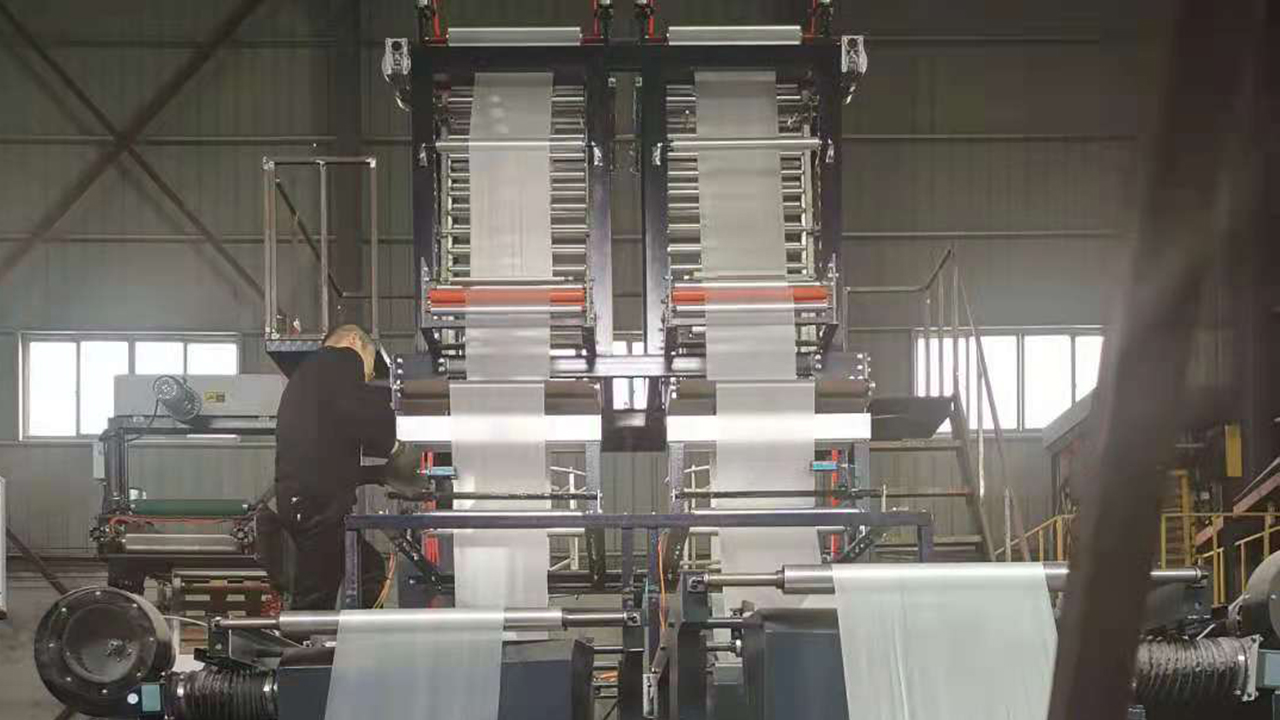
Multilayer blown film represents a sophisticated advancement in modern packaging technology that combines multiple layers of different materials into a single, unified film structure. This innovative multilayer blown film solution is manufactured through a specialized extrusion process where several polymer materials are simultaneously extruded and inflated into a bubble, then collapsed and wound onto rolls. Each layer within the multilayer blown film serves a specific function, working together to deliver superior performance characteristics that single-layer films cannot achieve. The technological features of multilayer blown film include precise layer engineering, where manufacturers strategically position barrier layers, structural layers, and tie layers to optimize the film's properties. The multilayer blown film technology enables the creation of films with exceptional oxygen barriers, moisture protection, puncture resistance, and shelf-life extension capabilities. This advanced manufacturing process allows producers to customize the multilayer blown film to meet specific application requirements without compromising on performance or cost-effectiveness. Applications for multilayer blown film are extensive and diverse. Industries including food packaging, pharmaceutical protection, agricultural covers, and industrial applications rely heavily on multilayer blown film products. The multilayer blown film performs exceptionally well in demanding environments where conventional films fail, providing reliable protection for perishable goods, sensitive medications, and other valuable products. Manufacturers value multilayer blown film for its versatility, allowing them to create customized solutions that address unique packaging challenges while maintaining rigorous quality standards.
New Product Releases

Multilayer blown film delivers exceptional value to businesses seeking reliable, high-performance packaging solutions that protect products while managing costs effectively. The primary advantage of multilayer blown film lies in its superior barrier protection, which dramatically extends product shelf life by preventing oxygen infiltration and moisture transmission. Customers benefit from reduced product spoilage, minimized waste, and increased consumer satisfaction through maintained product quality. Operational efficiency represents another critical advantage of multilayer blown film technology. Manufacturers can process multilayer blown film at high speeds on existing equipment without requiring significant capital investments in new machinery. The multilayer blown film reduces production complexity while improving output rates, directly translating to lower per-unit packaging costs and enhanced profitability for businesses of all sizes. The versatility of multilayer blown film makes it suitable for virtually any packaging application. Whether protecting fresh produce, frozen foods, pharmaceutical products, or industrial components, multilayer blown film adapts seamlessly to diverse requirements. Businesses appreciate how multilayer blown film simplifies supply chain management by consolidating multiple packaging types into single, standardized solutions. Sustainability benefits emerge as businesses increasingly adopt multilayer blown film alternatives. By maximizing product protection and minimizing waste, multilayer blown film reduces overall environmental impact compared to traditional single-layer options. The material efficiency of multilayer blown film means companies use less total plastic while achieving superior performance. Decision-making becomes straightforward when evaluating multilayer blown film options. The technology demonstrates proven reliability across thousands of manufacturing operations worldwide, with extensive documentation of performance metrics and application successes. Investment in multilayer blown film represents a strategic choice for forward-thinking companies prioritizing product quality, operational efficiency, and long-term profitability.

Latest News

Setting Up a PP Blown Film Machine: Step-by-Step Guide

13

May

Setting Up a PP Blown Film Machine: Step-by-Step Guide

Polypropylene (PP) film, due to its high transparency, strength, and heat resistance, is widely used in food packaging, daily necessities, pharmaceuticals, textiles, and other fields. During the production process, correct setup of the PP film blowin...
View More
How Automation Is Reshaping Plastic Bag Making Machine Efficiency

31

Jan

How Automation Is Reshaping Plastic Bag Making Machine Efficiency

Core Automation Technologies Driving Machine Efficiency Servo Motor Integration for Precision Speed Control and Energy Optimization Today's plastic bag manufacturing equipment relies on servo motor technology to get better control over speed and sa...
View More
Configuration of Blown Film Extruders for Uniform and High-Quality Plastic Film Production

27

Mar

Configuration of Blown Film Extruders for Uniform and High-Quality Plastic Film Production

Core Components of Blown Film Extruders and Their Impact on Melt Uniformity Screw Geometry and Compression Ratio: Balancing Shear, Mixing, and Melt Homogeneity How screws are designed plays a big role in achieving consistent melt quality during bl...
View More
Optimizing Film Thickness Control in Blowing Film Machines for Flexible Packaging Film Requirements

27

Mar

Optimizing Film Thickness Control in Blowing Film Machines for Flexible Packaging Film Requirements

Why Film Thickness Control Directly Determines Packaging Performance Mechanical strength loss from ±8% thickness variation in heat-seal layers When film thickness isn't consistent, particularly when heat seal layers vary more than about 8%, it...
View More

Let Us Help You with Pricing

Our sales team will contact you shortly with pricing details and suggestions.
Name
Company Name
Email
Mobile
Message
0/1000

multilayer blown film

Advanced Barrier Technology for Extended Product Protection

Advanced Barrier Technology for Extended Product Protection

Multilayer blown film incorporates sophisticated barrier layer engineering that creates an impermeable shield against oxygen, moisture, and light penetration. This multilayer blown film barrier technology utilizes specialized polymer combinations, strategically positioned within the film structure to maximize protection effectiveness. The result is dramatically extended shelf life for packaged products, reducing spoilage rates and improving retailer-consumer satisfaction significantly. The advanced barrier properties of multilayer blown film prove invaluable for temperature-sensitive items, premium products, and goods requiring extended distribution across global supply chains. Manufacturers implementing multilayer blown film solutions report measurable reductions in product returns, customer complaints, and waste-related losses. The investment in multilayer blown film technology delivers quantifiable returns through preserved product integrity and enhanced brand reputation, making it an essential choice for quality-conscious businesses.
Cost-Effective Manufacturing with Optimized Performance

Cost-Effective Manufacturing with Optimized Performance

Multilayer blown film technology achieves remarkable cost efficiency by combining multiple functional layers into a single production process, eliminating the need for complex lamination or co-extrusion procedures. This streamlined approach to multilayer blown film manufacturing reduces labor requirements, energy consumption, and equipment maintenance costs significantly. Businesses transitioning to multilayer blown film experience immediate operational cost reductions while maintaining or improving product protection capabilities. The production flexibility of multilayer blown film allows manufacturers to customize specifications precisely, minimizing material waste and maximizing resource utilization. Speed and consistency in multilayer blown film manufacturing enable high-volume production without quality compromises. Companies benefit from predictable costs, reliable supply chains, and competitive pricing advantages when adopting multilayer blown film solutions. This combination of performance excellence and economic efficiency makes multilayer blown film the preferred choice for manufacturers seeking sustainable profitability.
Versatile Applications Across Multiple Industries

Versatile Applications Across Multiple Industries

Multilayer blown film demonstrates remarkable adaptability across diverse packaging applications, from food and beverages to pharmaceuticals and industrial products. The engineered design of multilayer blown film accommodates specific requirements of different industries without requiring complete production line redesigns. This versatility of multilayer blown film simplifies inventory management, reduces SKU complexity, and streamlines procurement processes for multi-sector organizations. Businesses leveraging multilayer blown film technology gain competitive advantages through standardized, high-performance packaging solutions applicable across product portfolios. The multilayer blown film performs exceptionally under varied storage conditions, temperature fluctuations, and environmental stresses that challenge conventional alternatives. Organizations benefit from streamlined operations, reduced supply chain fragmentation, and improved vendor relationships when consolidating packaging needs around multilayer blown film technology, ultimately enhancing operational efficiency and market responsiveness.