Blown Film Products: Flexible Packaging Solutions

Let Us Help You with Pricing

Our sales team will contact you shortly with pricing details and suggestions.
Name
Company Name
Email
Mobile
Message
0/1000

blown film products

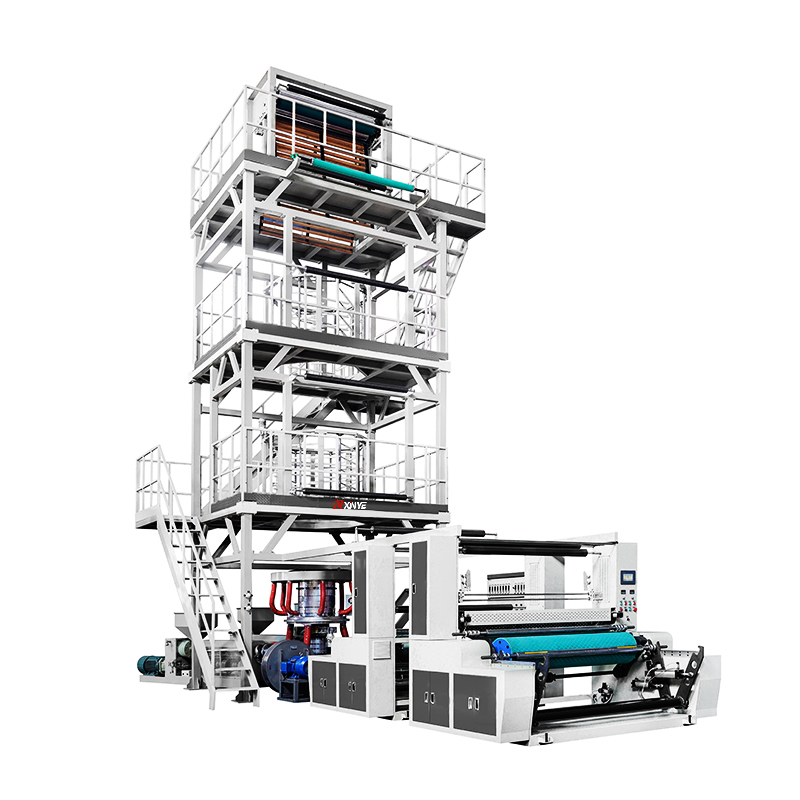
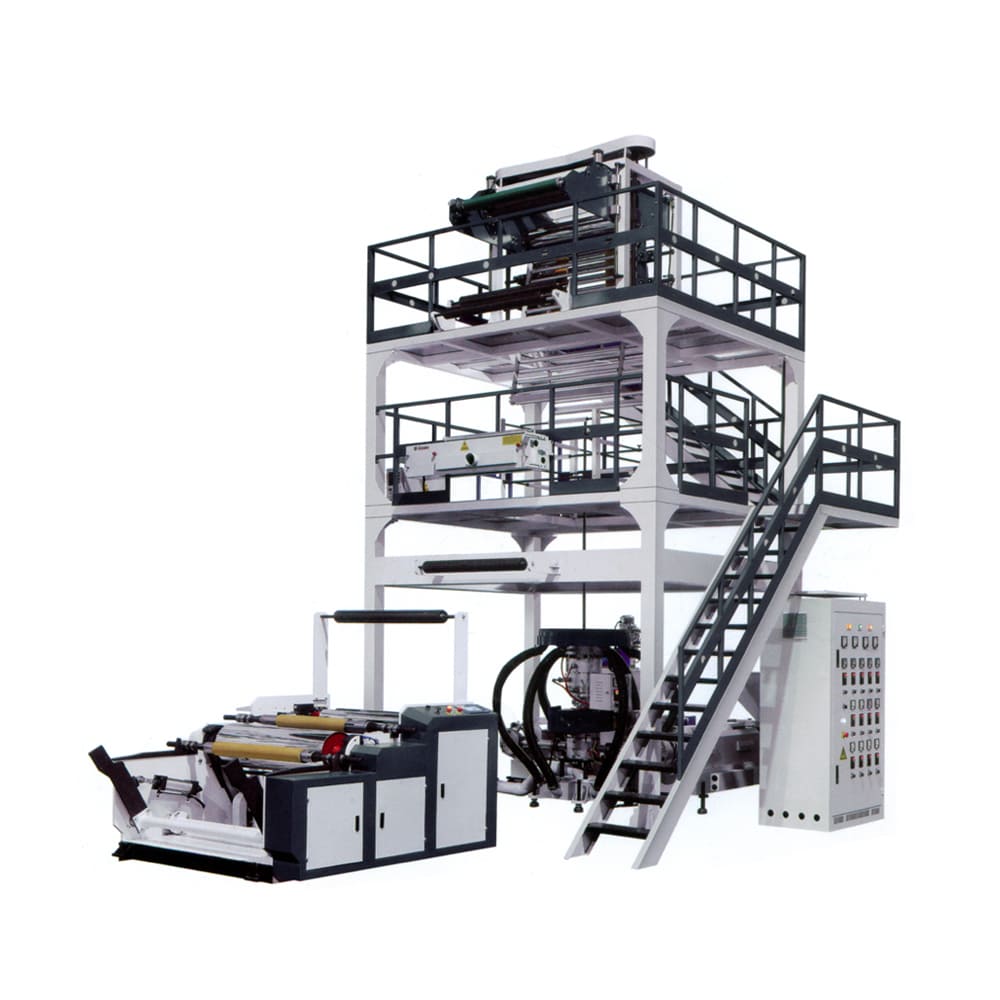
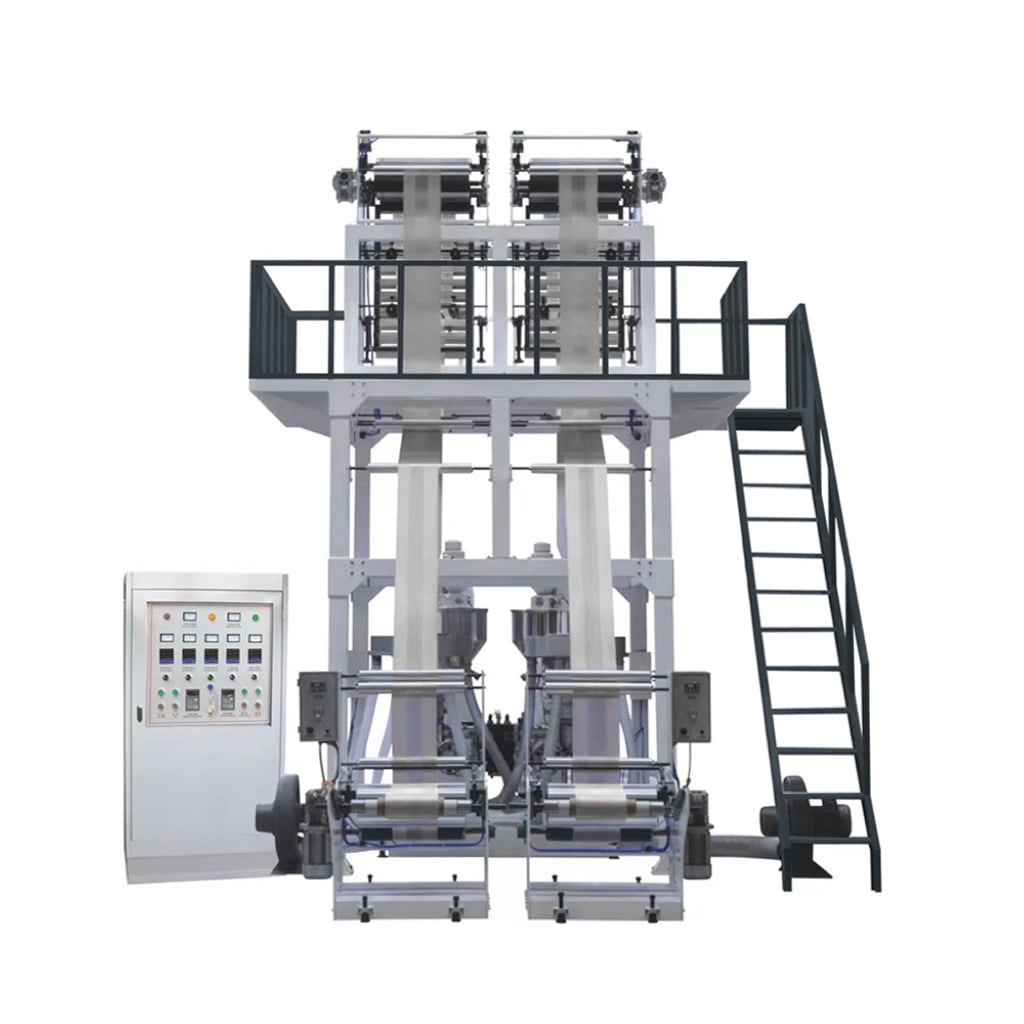
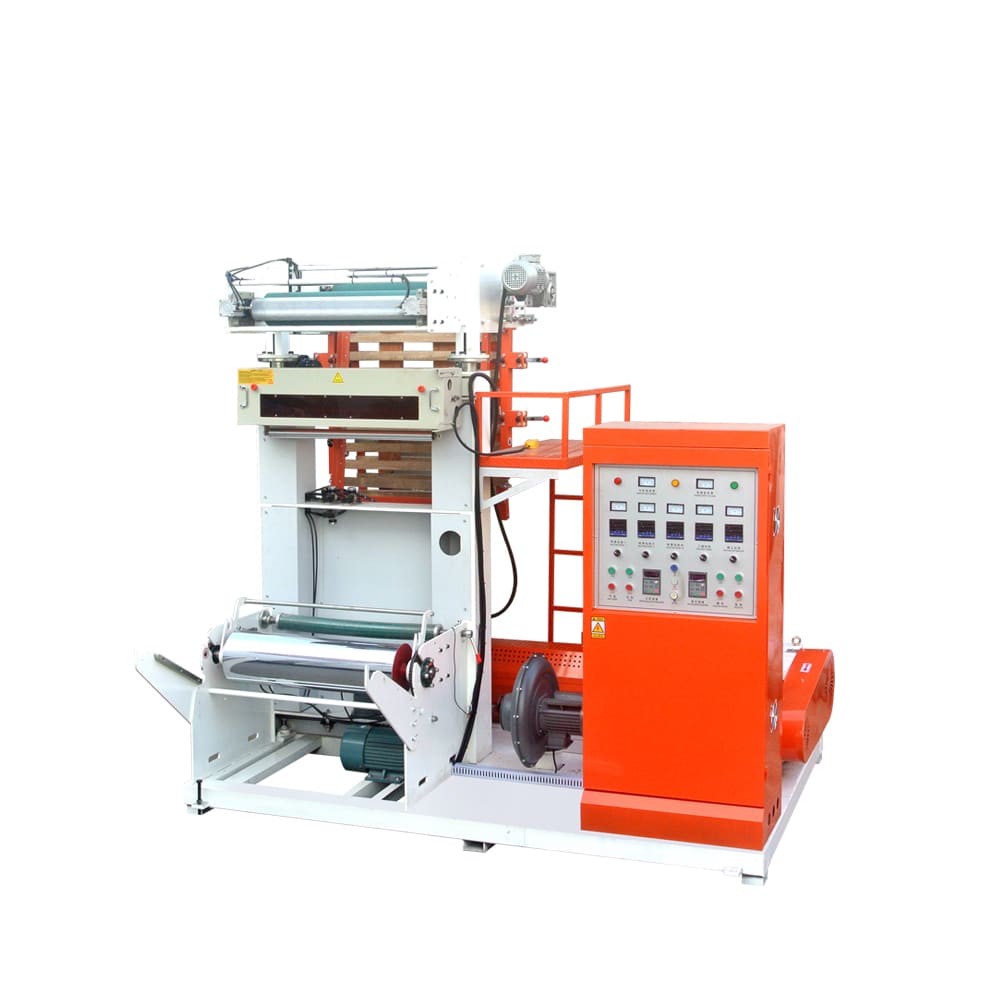
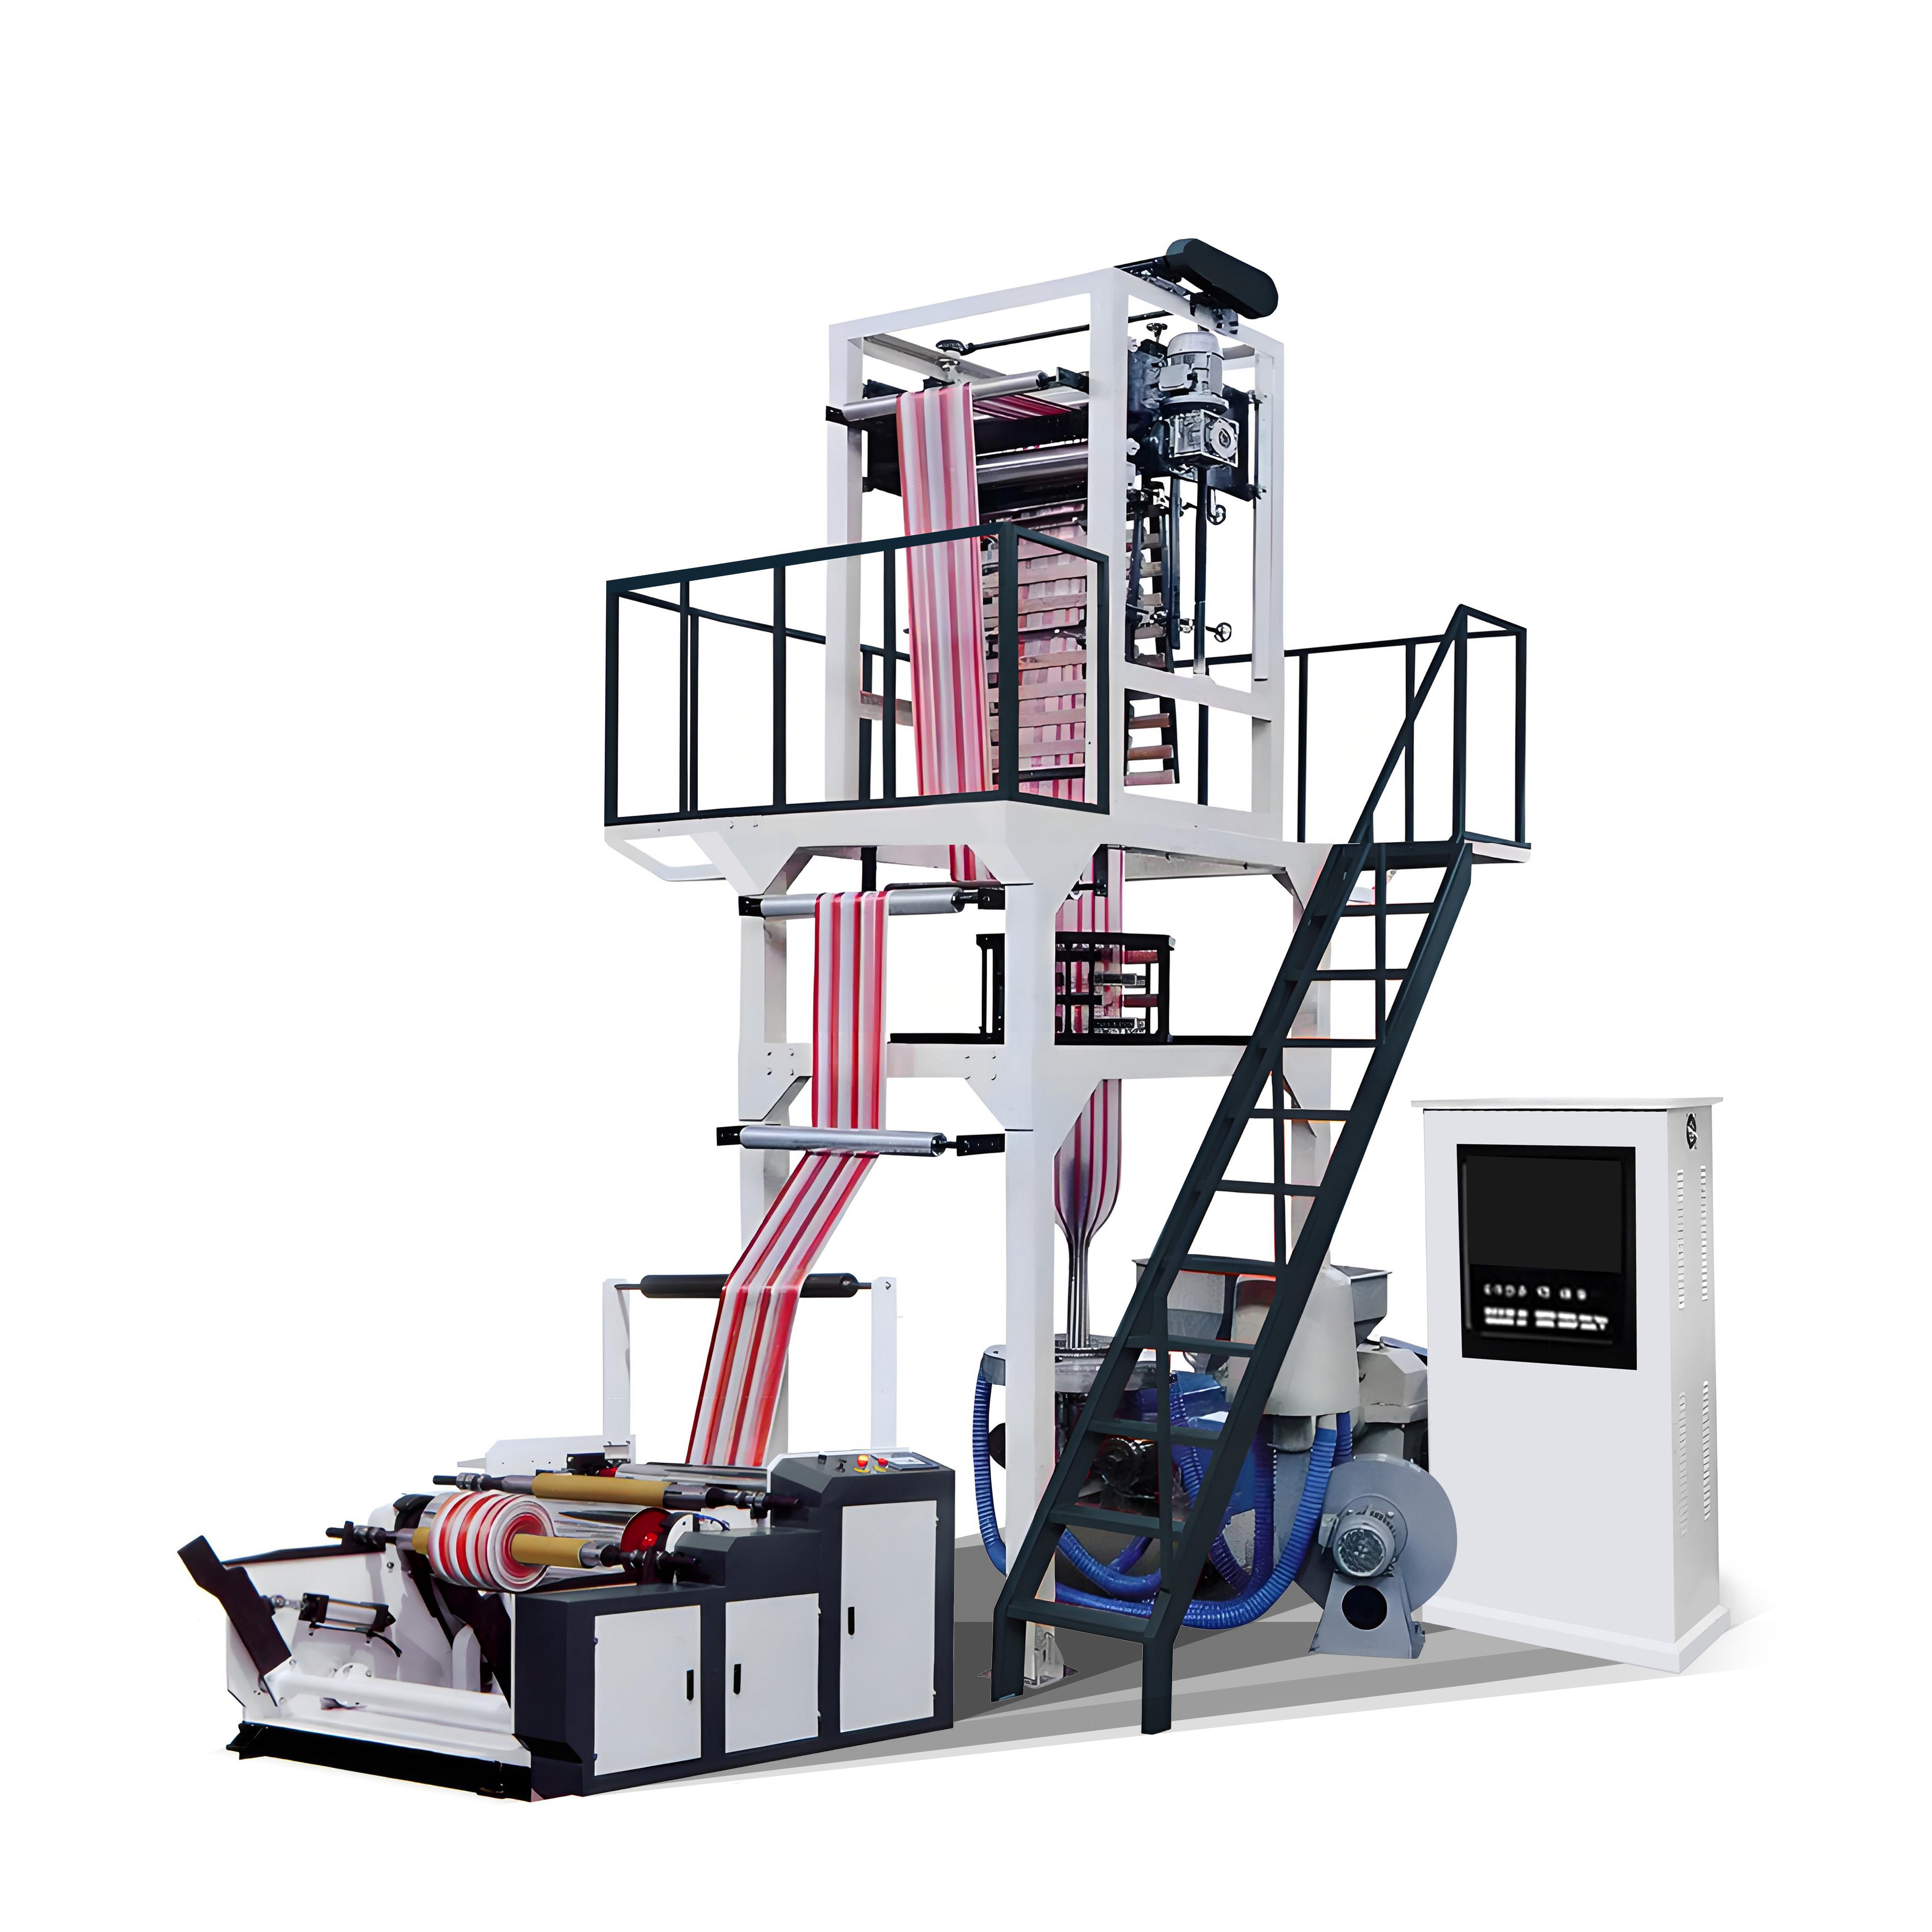
Blown film products represent a sophisticated plastic film production technology that manufactures thin, flexible sheets through an extrusion and inflation process. These blown film products are created by forcing molten plastic through a circular die, then inflating the resulting tube with air to achieve the desired thickness and width. The primary function of blown film products is to provide protective, flexible packaging solutions across numerous industries. The technological features of blown film products include precise temperature control, advanced extrusion systems, and inflation mechanisms that ensure consistent quality and performance. These blown film products demonstrate exceptional tensile strength, puncture resistance, and flexibility, making them ideal for demanding applications. The manufacturing process of blown film products allows for customization of film thickness, width, and material composition to meet specific customer requirements. Common applications for blown film products include food packaging, agricultural films, industrial wrapping, and protective coverings. Blown film products excel in creating moisture barriers, oxygen barriers, and protective layers that extend product shelf life and maintain integrity during storage and transportation. The versatility of blown film products stems from their ability to incorporate multiple material layers, enabling enhanced barrier properties and functional performance. Modern blown film products can integrate additives for UV protection, anti-static properties, and enhanced durability. The production of blown film products continues to advance with innovations in polymer technology and manufacturing efficiency. Industries worldwide depend on blown film products for reliable, cost-effective packaging and protection solutions that meet rigorous quality standards and regulatory compliance requirements.
New Product Releases

Blown film products deliver exceptional practical benefits that make them the preferred choice for businesses seeking reliable packaging and protective solutions. These products offer outstanding flexibility and durability, allowing them to conform to various product shapes while resisting punctures and tears during handling and transportation. The lightweight nature of blown film products significantly reduces shipping costs and environmental impact compared to heavier alternative materials. Customers benefit from the superior moisture and oxygen barrier capabilities that blown film products provide, ensuring products remain fresh and protected throughout their shelf life. Operational advantages include seamless integration with existing packaging equipment, minimizing implementation costs and production downtime. Blown film products enable manufacturers to achieve cost-effective production runs with minimal material waste, directly improving profit margins. The customization capabilities of blown film products allow businesses to create branded packaging that enhances market appeal and consumer recognition. These products demonstrate exceptional clarity and printability, supporting marketing objectives and product visibility on retail shelves. Blown film products provide proven reliability across food, pharmaceutical, agricultural, and industrial sectors, demonstrating their broad application suitability. The thermal stability of blown film products ensures consistent performance across diverse environmental conditions and temperature ranges. For businesses prioritizing sustainability, blown film products offer recyclability options and opportunities for reduced plastic consumption through optimized thickness. The scalability of blown film products manufacturing supports everything from small batch productions to large-scale industrial operations. Decision-makers appreciate that blown film products meet stringent regulatory requirements and quality standards worldwide, reducing compliance concerns. The excellent heat seal properties found in blown film products enable secure package closure without additional fastening methods. Industries consistently choose blown film products for their proven performance record, cost efficiency, and ability to address complex packaging challenges effectively.

Latest News

How to Improve Production Speed on a Plastic Bag Making Machine

26

Dec

How to Improve Production Speed on a Plastic Bag Making Machine

Optimizing Mechanical Settings for Higher Throughput in Plastic Bag Making Machines Fine-Tuning Film Tension and Sealing Temperature Getting the right amount of tension in the film is really important when running at high speeds. If there's not en...
View More
The Role of Film Thickness Control in High-Quality Blown Film Production

31

Jan

The Role of Film Thickness Control in High-Quality Blown Film Production

Why Film Thickness Control Is Fundamental to Blown Film Quality How thickness uniformity directly determines mechanical strength, optical clarity, and barrier performance Getting film thickness just right matters a lot for blown film quality becaus...
View More
How Automation Is Reshaping Plastic Bag Making Machine Efficiency

31

Jan

How Automation Is Reshaping Plastic Bag Making Machine Efficiency

Core Automation Technologies Driving Machine Efficiency Servo Motor Integration for Precision Speed Control and Energy Optimization Today's plastic bag manufacturing equipment relies on servo motor technology to get better control over speed and sa...
View More
Tower Design Considerations in High-Speed Film Blowing Equipment

25

Feb

Tower Design Considerations in High-Speed Film Blowing Equipment

Structural Integrity and Dynamic Stability of the Film Blowing Tower Managing Dynamic Loads and Vibration at High Line Speeds When running at over 100 meters per minute, film blowing towers encounter all sorts of dynamic problems that can really s...
View More

Let Us Help You with Pricing

Our sales team will contact you shortly with pricing details and suggestions.
Name
Company Name
Email
Mobile
Message
0/1000

blown film products

Superior Barrier Protection Technology

Superior Barrier Protection Technology

Blown film products incorporate advanced barrier technology that protects contents from external environmental factors including moisture, oxygen, light, and contaminants. This multi-layer barrier capability ensures products maintain optimal freshness, potency, and quality throughout their entire shelf life. The barrier properties of blown film products prevent degradation caused by oxidation, moisture absorption, and light exposure, making them essential for sensitive products like food, pharmaceuticals, and chemicals. Manufacturers can customize the barrier specifications of blown film products by selecting appropriate polymer combinations and layer configurations. The effectiveness of blown film products in maintaining product integrity reduces waste, extends marketability, and increases customer satisfaction. Modern blown film products achieve barrier performance comparable to rigid packaging while maintaining the cost advantages and flexibility benefits of film solutions. The oxygen transmission rates of blown film products can be precisely controlled to match specific product requirements and industry standards. Businesses utilizing blown film products experience reduced product spoilage, returns, and customer complaints related to quality degradation. The transparency of blown film products allows consumers to view products while maintaining complete protection from environmental elements. These protective capabilities make blown film products indispensable for industries where product preservation directly impacts profitability and brand reputation.
Cost-Effective Production Efficiency

Cost-Effective Production Efficiency

Blown film products deliver remarkable economic advantages through streamlined manufacturing processes and minimal material waste. The production efficiency of blown film products reduces operational costs substantially compared to alternative packaging methods and traditional materials. Manufacturing blown film products requires less energy input than many competitive packaging solutions, directly lowering production expenses and environmental footprint. The high-speed production capability of blown film products enables manufacturers to meet large volume demands without proportional increases in overhead costs. Waste reduction during blown film products manufacturing contributes significantly to overall profitability by maximizing material utilization rates. The versatility of blown film products allows producers to manufacture multiple product specifications using similar equipment, improving operational flexibility and reducing capital requirements. Suppliers of blown film products offer competitive pricing while maintaining quality standards, creating favorable procurement conditions for volume buyers. The lightweight characteristics of blown film products reduce transportation expenses, warehouse storage requirements, and handling labor costs throughout distribution channels. Implementing blown film products eliminates costly secondary processing steps required by some alternative packaging solutions. The durability of blown film products minimizes damage-related losses and replacement costs during storage and distribution phases. Companies transitioning to blown film products consistently report improved cost structure and enhanced competitive positioning in their respective markets.
Versatile Multi-Application Performance

Versatile Multi-Application Performance

Blown film products demonstrate exceptional versatility across virtually every industrial sector requiring protective packaging and flexible film solutions. The adaptability of blown film products extends from fresh food packaging to agricultural coverings, industrial wrapping, medical applications, and heavy-duty industrial uses. Pharmaceutical companies rely on blown film products for protecting sensitive medications and medical devices requiring precise barrier properties and contamination prevention. Agricultural industries utilize blown film products for greenhouse coverings, crop protection films, and produce packaging that extends harvest season profitability. The food packaging sector depends on blown film products to maintain freshness, prevent spoilage, and meet strict food safety regulations and standards. Manufacturing environments benefit from blown film products applications in protective coverings, equipment wrapping, and corrosion prevention solutions. Construction industries employ blown film products for moisture barriers, dust protection, and temporary weather shielding during building projects. The consistent performance of blown film products across diverse applications demonstrates their universal reliability and superior engineering design. Customization options available with blown film products allow specific adaptations for unique industry requirements and specialized use cases. Food service operations, retail environments, and logistics companies all depend on blown film products for efficient, cost-effective packaging solutions. The proven track record of blown film products across multiple industries validates their effectiveness, safety, and compliance with applicable regulations and standards.